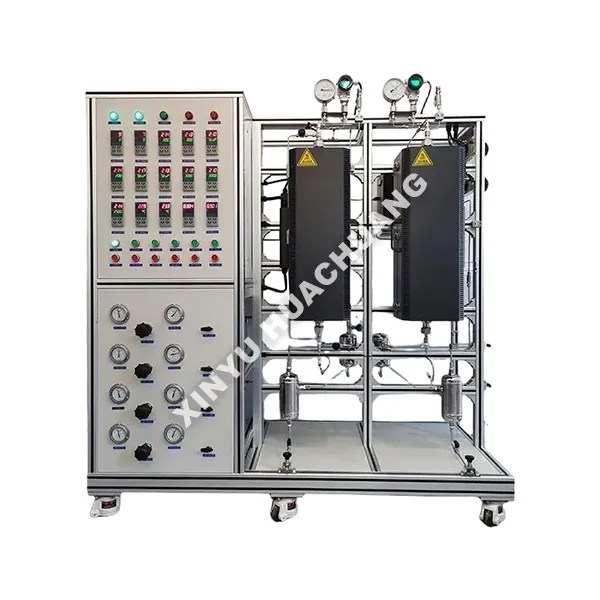
TIANJIN XINYUHUACHUANG TECHNOLOGY CO., LTD. (XINYU HUACHUANG) is a technology-driven enterprise integrating R&D, design, manufacturing, and sales. Established in 2017 with a registered capital of RMB 10 million, our company is located in the Huigu Industrial Park within the Tiankai Xiqing Zone, Tianjin. Leveraging the research resources of prestigious universities—such as Tianjin University and Nankai University (institutions included in China’s "Project 985," "Project 211," and the "Double First-Class" initiative)—our company specializes in the manufacturing of reaction units, rectification and separation units, coal chemical equipment, laboratory distillation apparatus, and custom non-standard equipment. Its expertise also extends to the development, design, and production of pilot-scale platforms, as well as the design and development of process packages.
Our company’s business scope spans numerous industrial sectors, including petrochemicals, coal chemicals, fine chemicals, fluorochemicals, environmental engineering, chemical automation, organic and polymer synthesis, solvent recovery, biopharmaceuticals, and wastewater treatment.
Since its inception, XINYU HUACHUANG has adhered to principles of integrity and trustworthiness, grounded in a philosophy of pragmatic operation and outstanding innovation. By prioritizing customer needs, centering on technology, and guaranteeing quality, our company delivers high-quality services to its diverse clientele.
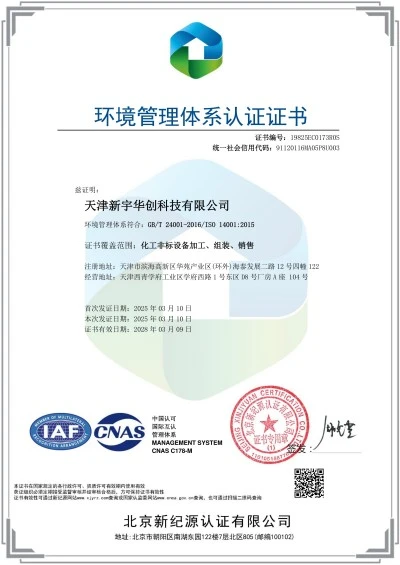
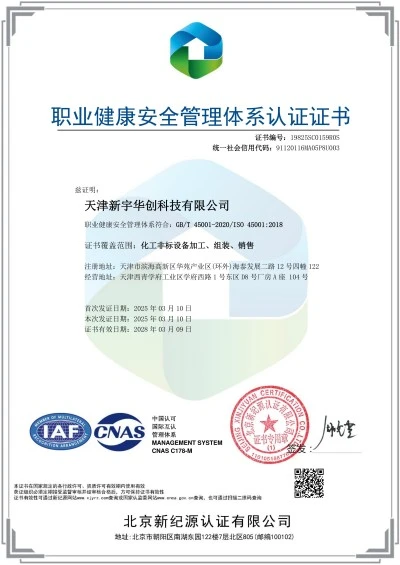
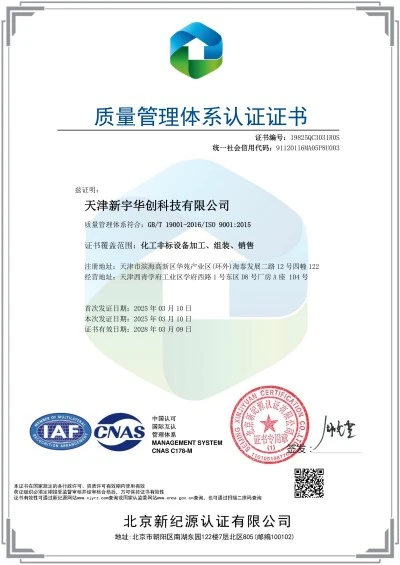
Our company holds certifications for the ISO9001, ISO14001, and ISO45001 management systems, as well as the High-Tech Enterprise certification.
With a professional design team, superb manufacturing techniques, a comprehensive management system, and high-quality, timely after-sales service, our company serves numerous research institutes, universities, and enterprises, earning an excellent reputation and widespread acclaim.
Our History
2017
Our company was established, initially focusing on reaction and fractional distillation units. Leveraging the cutting‑edge research resources and national‑level laboratory platforms of Tianjin University and Nankai University—both among China’s first "Project 985," "Project 211," and "Double First‑Class" (Class A) universities—we deeply integrated their frontier research achievements in fields such as chemical process intensification, catalytic reaction engineering, and separation technology. We successfully entered the market for chemical experimental equipment and complete process units.
2019‑2020
We launched our first core products, including catalyst evaluation units and laboratory distillation columns, with business operations spanning sectors such as petrochemicals, fine chemicals, and fluorochemicals.
2021‑2022
Our product line expanded to include pilot‑scale reaction units, fluidized bed evaluation units, fixed‑bed reaction units, and high‑pressure hydrogenation reactors. We secured a total of 19 utility model patents and achieved ISO "Three‑System" certification.
2023‑Present
Driven by continuous technological innovation and robust R&D capabilities, we were officially recognized as a National High‑Tech Enterprise. Our core clientele includes top domestic universities, national research institutes, and industry leaders. These include Tianjin University ("Double First‑Class" Class A); Haohua Gas Co., Ltd. (a leader in specialty gases under the Fortune Global 500 company Sinochem); Beijing OriginWater Membrane Technology Co., Ltd. (a benchmark enterprise in China's environmental water industry and a "Global Top 50 Water Company"); Solvay Chemical (Shanghai) Co., Ltd. (a comprehensive chemical group); Xi'an Modern Chemistry Research Institute (China's research center for energetic chemical materials under Norinco Group); and Liming Chemical Research Institute Co., Ltd. (under Sinochem). These partnerships fully demonstrate our technical prowess and market recognition in the field of chemical experimental equipment and complete process units.
Our Factory
TIANJIN XINYUHUACHUANG TECHNOLOGY CO., LTD. boasts standardized production strength and standardized quality management, supporting customized manufacturing and stable bulk delivery of chemical and scientific research equipment. Our core factory strengths are detailed as follows:
Established in 2017, the company has a registered capital of 10 million RMB, with an independent 1,500 ㎡ professional production plant located in Huigu Industrial Park, Tianjin Tikai Xiqing Park. We integrate independent R&D, structural design, precision production and full after‑sales service.
The factory is equipped with 5 assembly production lines and 2 parts independent processing lines. We maintain a stable monthly output of over 10 sets of complete equipment, capable of meeting diversified, non‑standard customized and batch order delivery requirements.
We own a professional technical team with technical personnel accounting for 60% of all staff. Equipped with 5 full‑time professional quality inspectors, we implement strict whole‑process quality control covering raw material incoming inspection, in‑production processing monitoring and finished product factory inspection.
Relying on the scientific research resources of Tianjin University and Nankai University, we specialize in customized design and manufacturing of reaction devices, distillation separation equipment, coal chemical units and laboratory experimental equipment, as well as pilot platform development and process package design.
Product Application
Reaction Units
-
Catalyst evaluation units
-
fixed‑bed catalyst reaction units
-
pilot‑scale reaction units
-
high‑pressure hydrogenation reactor systems
Distillation & Separation Units
-
Laboratory distillation columns
-
skid‑mounted distillation units
-
column internals
Coal Chemical & Evaluation Units
-
Fluidized‑bed evaluation units
-
SCR dual‑reactor evaluation units
-
multi‑channel Fischer‑Tropsch synthesis units
-
methanol catalysis testing units
-
methane reforming experimental units
-
gasification and synthesis experimental units
-
adsorption‑desorption reaction units
Customized Solutions & Pilot Platforms
-
Process package design
-
pilot platform development and manufacturing
Our business scope spans numerous industrial sectors, including petrochemicals, coal chemicals, fine chemicals, fluorochemicals, environmental engineering, chemical automation, organic and polymer synthesis, solvent recovery, biopharmaceuticals, and wastewater treatment.
Certificate
Our company has obtained certifications for the ISO 9001, ISO 14001, and ISO 45001 management systems, as well as the High-Tech Enterprise certificate.
Production Equipment
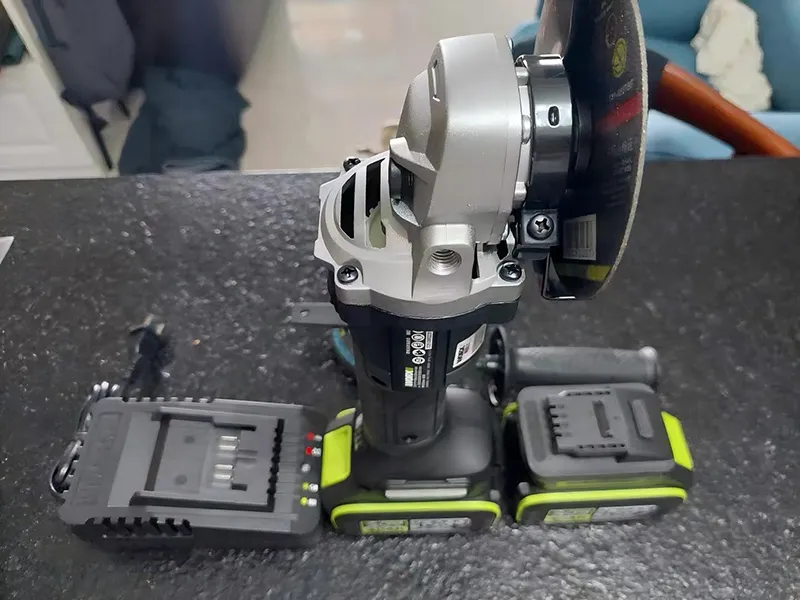
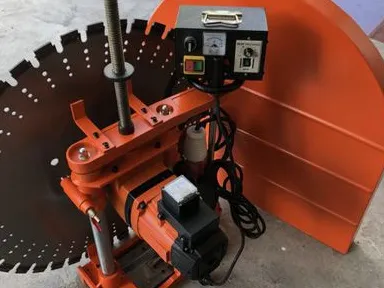
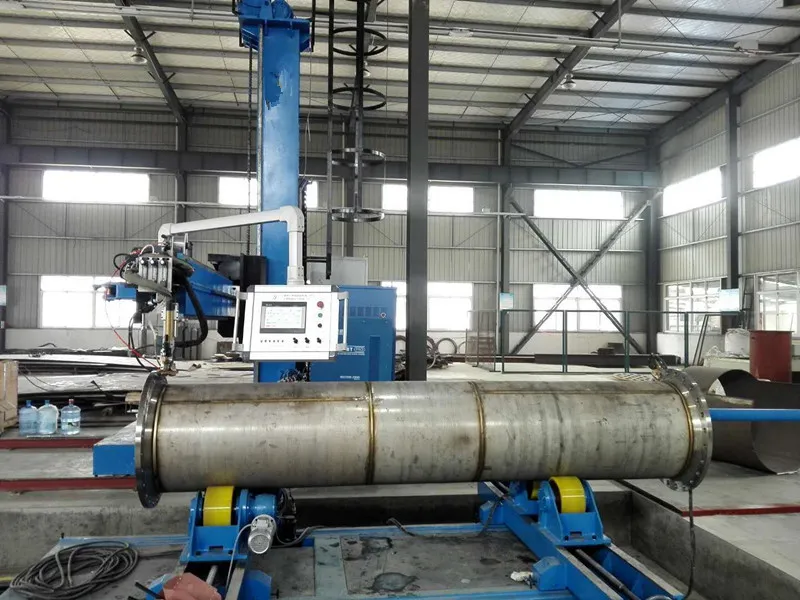
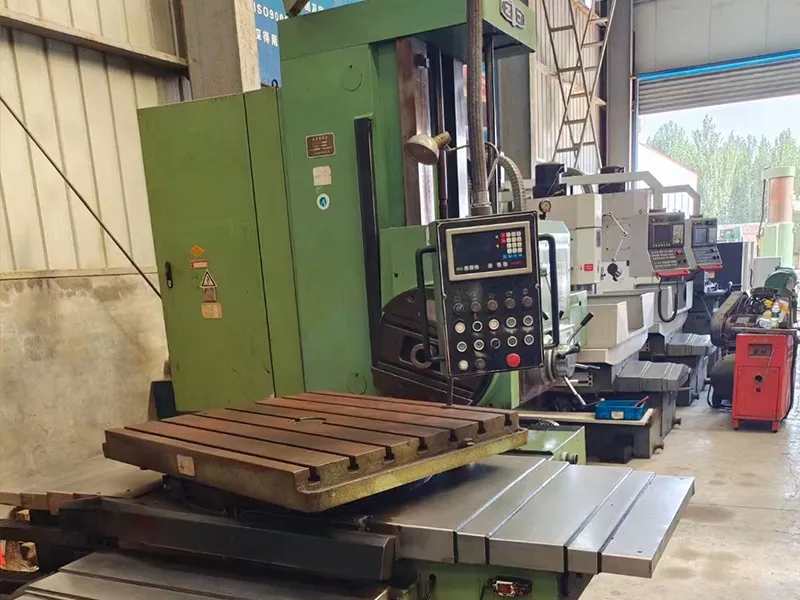
Argon arc welding machine; drilling, milling, and boring machine; water saw; angle grinder.
Our Exhibition
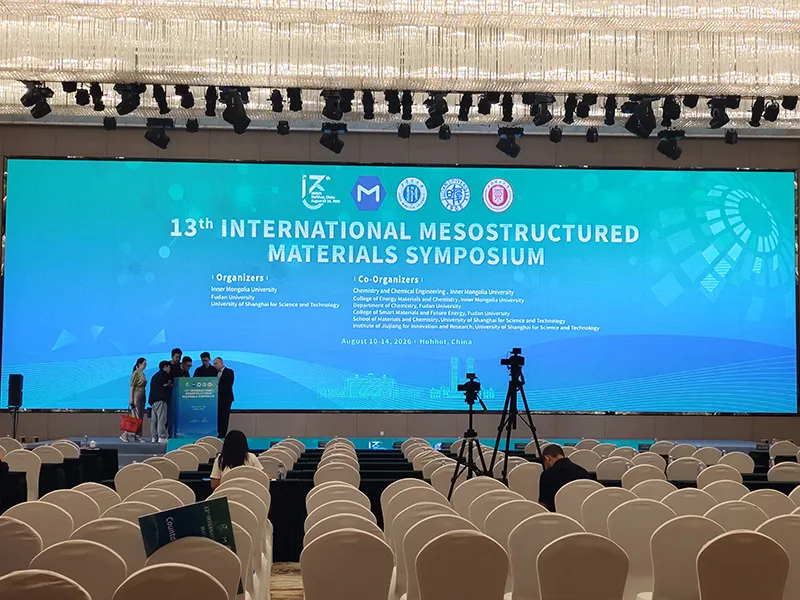
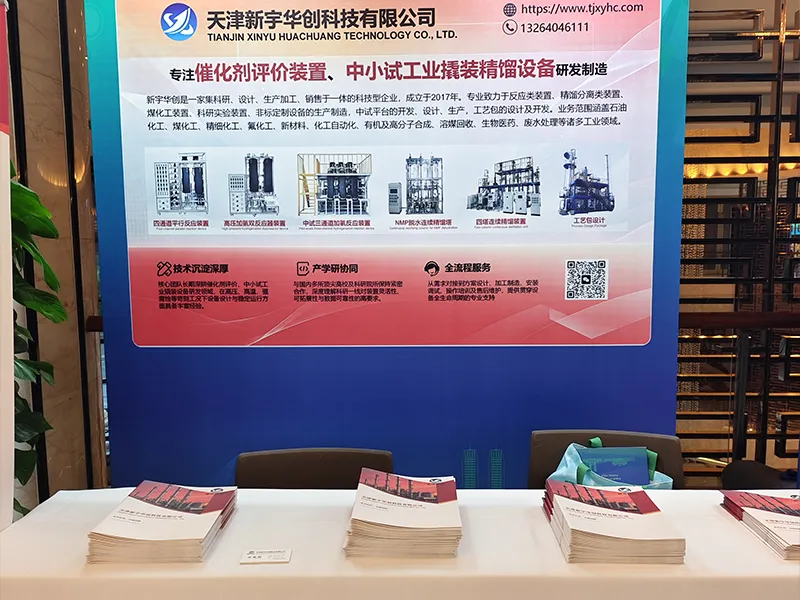
The 13th International Symposium on Mesostructured Materials