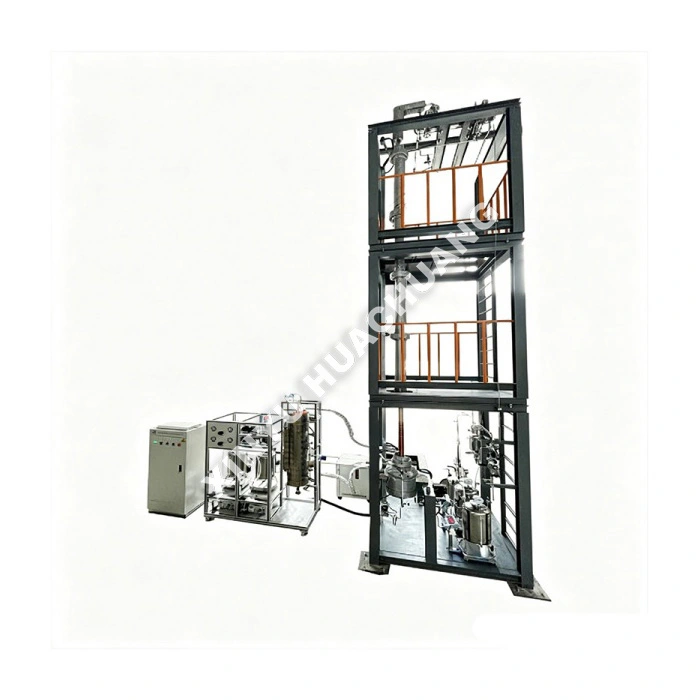
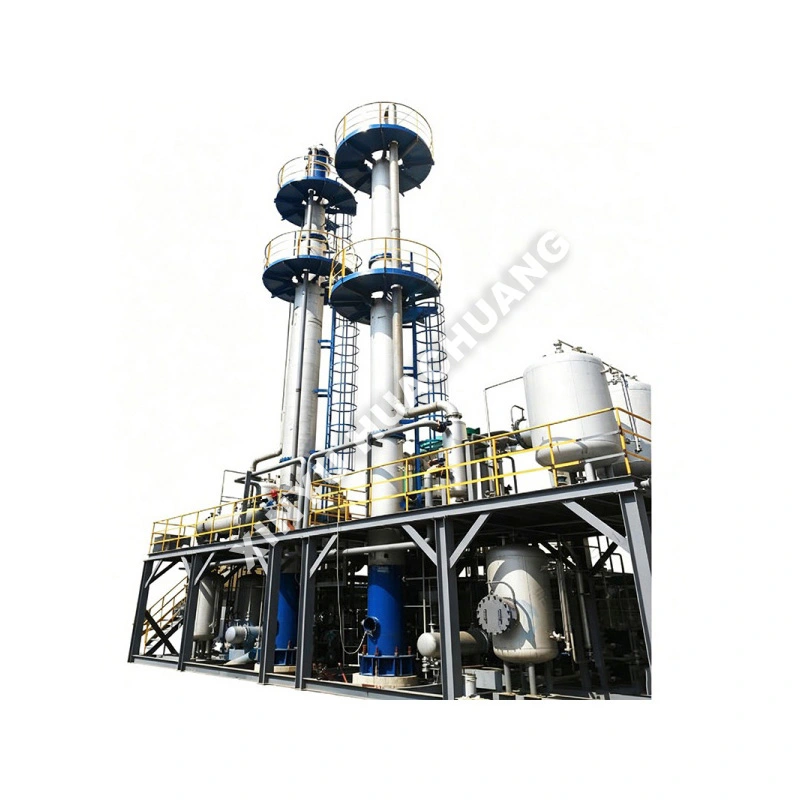
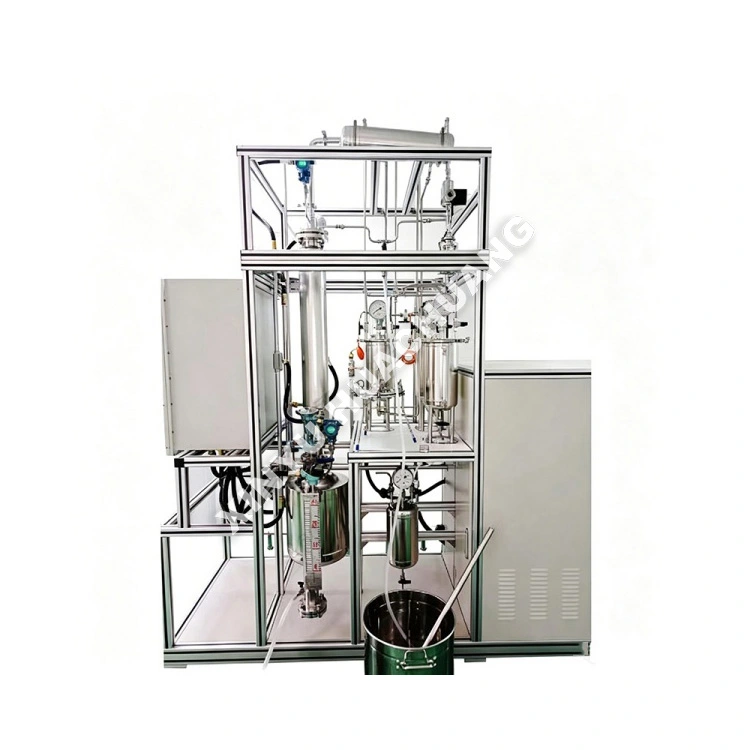
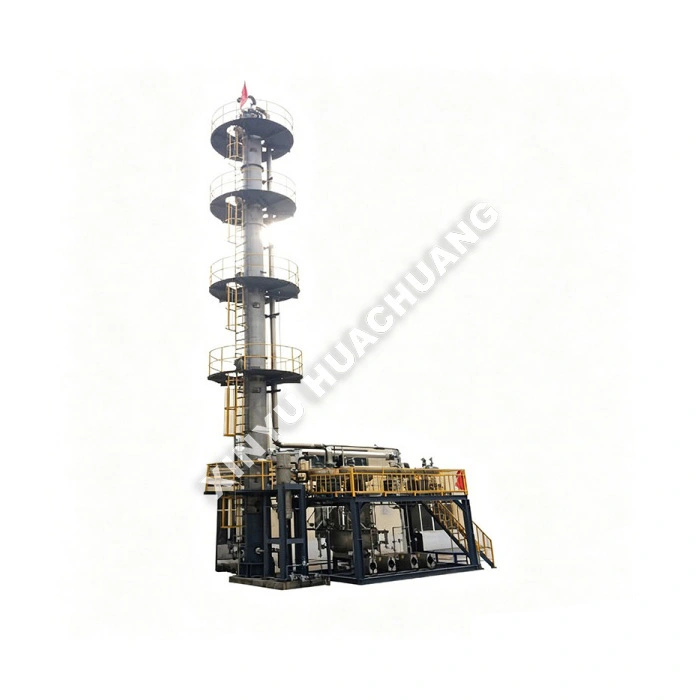
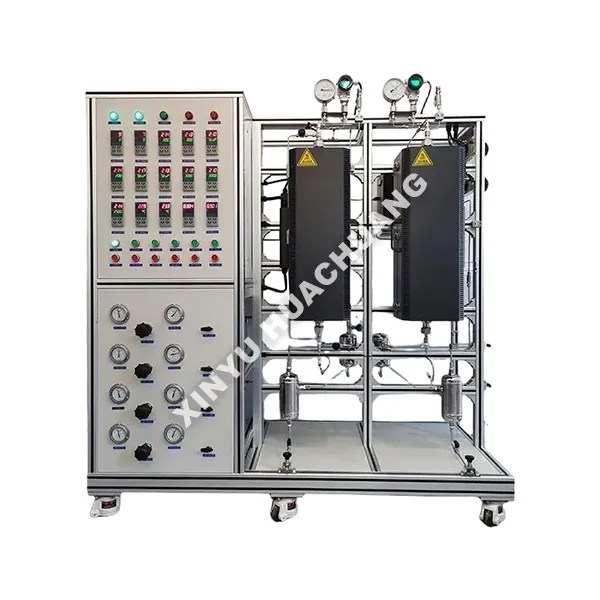
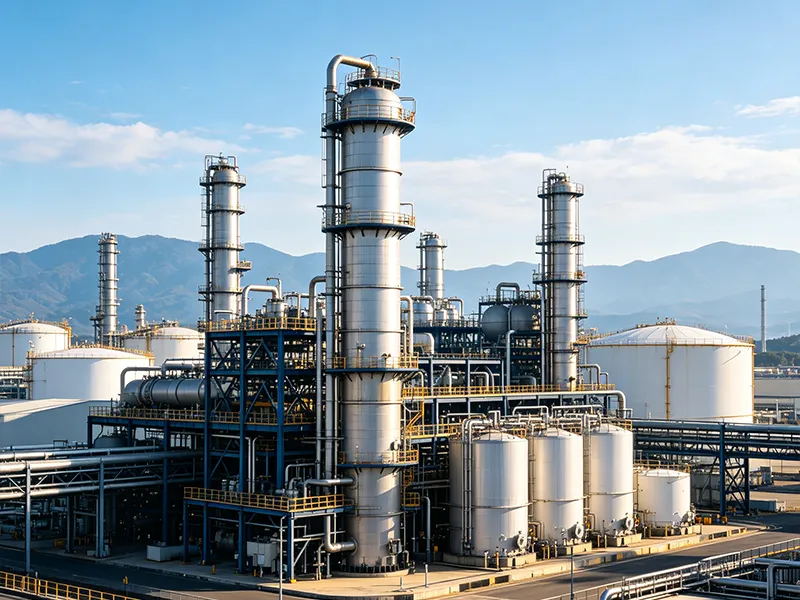
Recovery distillation units are distillation systems used to recover valuable solvents or liquid components from waste liquid, off-spec material, cleaning liquid, mother liquor or process by-product streams. These units typically include a reboiler, distillation column, column internals, condenser, reflux control, fraction collection section, temperature and pressure monitoring and safety protection devices.
They are suitable for solvent recycling, light-end recovery, heavy-residue separation, moisture removal, purity upgrading and small-batch solvent regeneration. The system can be configured for atmospheric, vacuum or combined operation according to the boiling point characteristics, thermal stability and recovery target of the processed liquid.
How Should a High-Quality Recovery Distillation Unit Be Selected?
A reliable recovery distillation unit should be selected based on actual liquid composition rather than capacity alone. Key factors include solvent type, impurity profile, boiling point difference, water content, corrosion risk, expected recovery rate, target purity and whether the recovered solvent will be reused directly or sent for further purification.
Material selection, column efficiency, heating method, condenser capacity and fraction collection design should all match the recovery scenario. For corrosive or high-purity recovery tasks, sealing structure and wetted material grade should be carefully confirmed. For heat-sensitive solvents, vacuum operation and controlled heating are usually preferred.
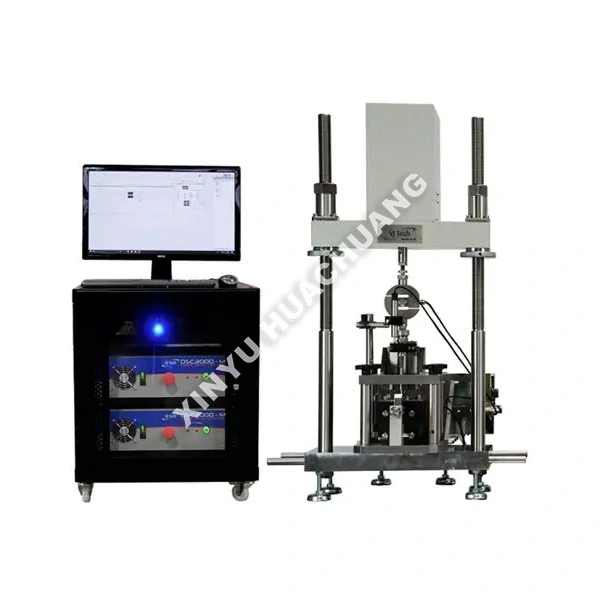
As a direct manufacturer of chemical experimental and pilot equipment, XINYU HUACHUANG provides practical recovery distillation design and solvent system matching, giving customers clearer process evaluation, more accurate recovery configuration, flexible adaptation to different solvent streams, and responsive technical support. In addition to Recovery Distillation Units, we also supply Fixed-bed and Multi-channel Catalyst Evaluation Devices, Hydroprocessing Pilot Reaction Units, Special-Material and Special-Grade Distillation Units, and Comprehensive Stress Test Bench.
What Is the Procurement Process?
The procurement process usually begins with process confirmation. Customers provide feed composition, solvent type, impurity information, boiling point range, expected throughput, recovery purity and installation requirements. Our team then reviews the recovery feasibility and prepares a configuration proposal.
After the proposal is confirmed, commercial terms, delivery time and technical documents are finalized. The unit then enters manufacturing, assembly, inspection and functional testing. Before shipment, we check equipment appearance, piping connections, instrument functions and accessory completeness. For international customers, export packaging, shipping coordination and related documents can be arranged according to the agreed contract terms.
Frequently Asked Questions
1. What types of waste liquid can be treated by recovery distillation?
Recovery distillation units can handle many solvent-containing liquids, including off-spec solvent, cleaning liquid, mother liquor and process by-product streams. Final feasibility depends on composition, boiling point relationship and thermal stability.
2. Can recovered solvents reach reuse grade?
Yes. Recovered solvents can often reach reuse grade when the column configuration, reflux control and fraction collection are properly matched. For higher purity requirements, additional polishing or secondary distillation may be considered.
3. How is recovery efficiency improved?
Recovery efficiency can be improved by optimizing reflux ratio, heating rate, vacuum level, fraction cutting strategy and column internals selection. Accurate feed analysis helps avoid unnecessary energy consumption and product loss.
4. Do you provide after-sales and technical support?
Yes. As the original manufacturer, we provide technical consultation, operation guidance, spare parts supply and after-sales service. For customized recovery distillation systems, we can also support customers with configuration confirmation, commissioning advice and maintenance recommendations.