Products
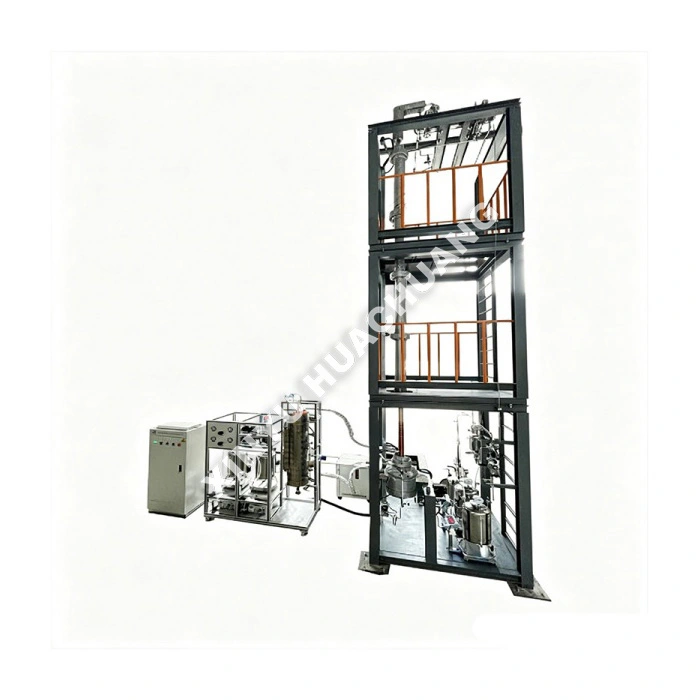
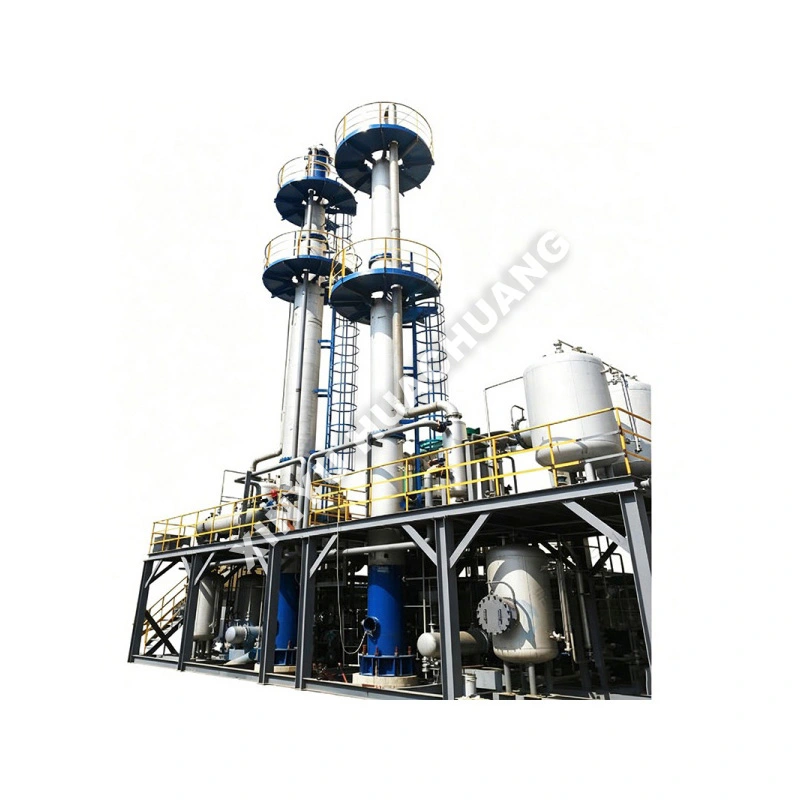
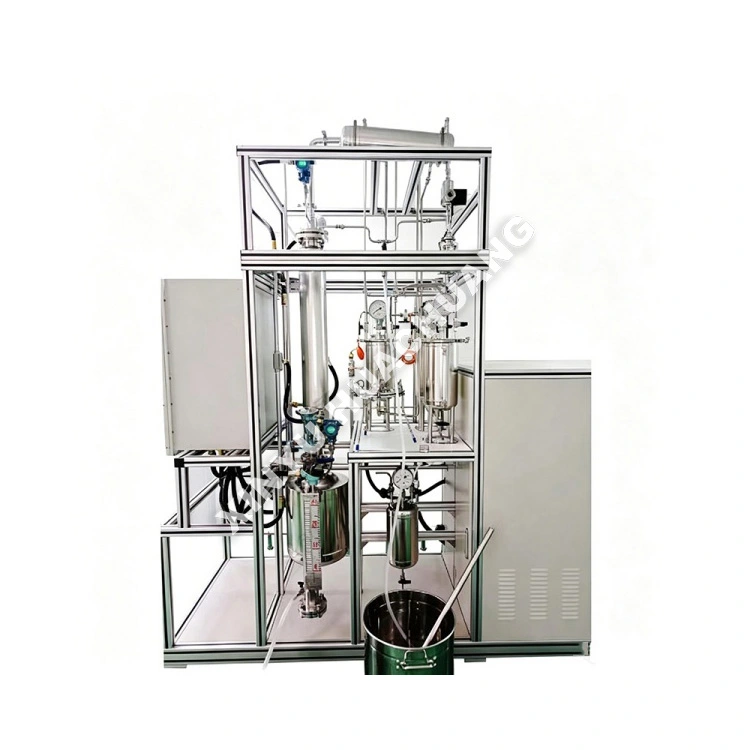
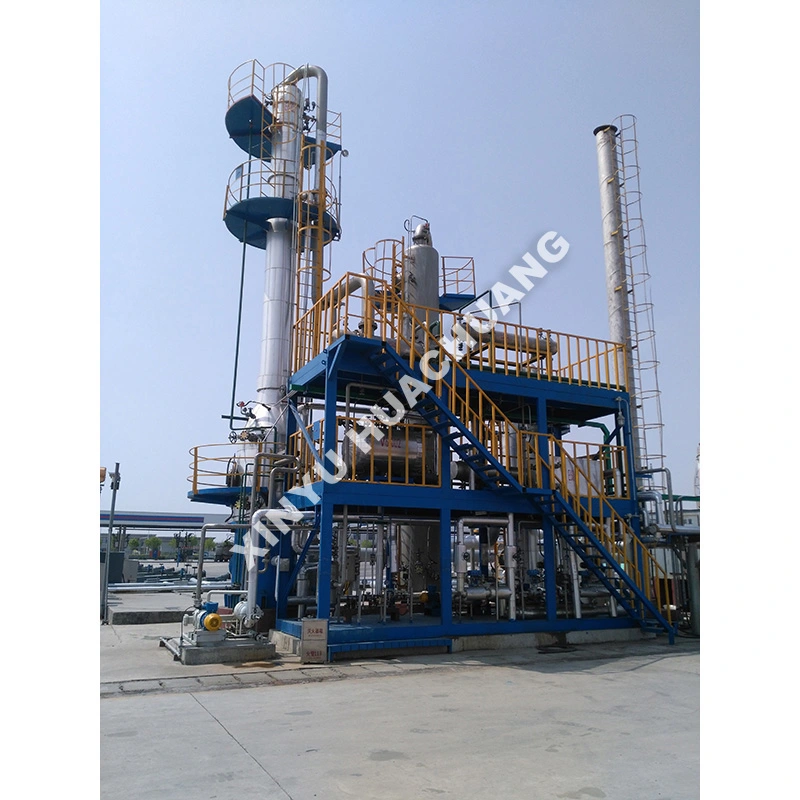
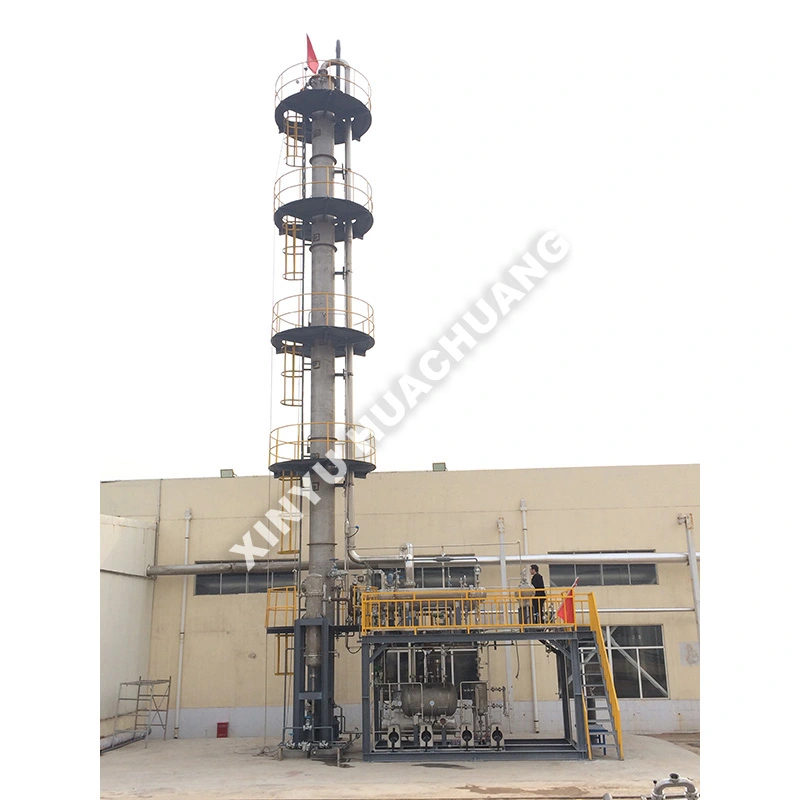
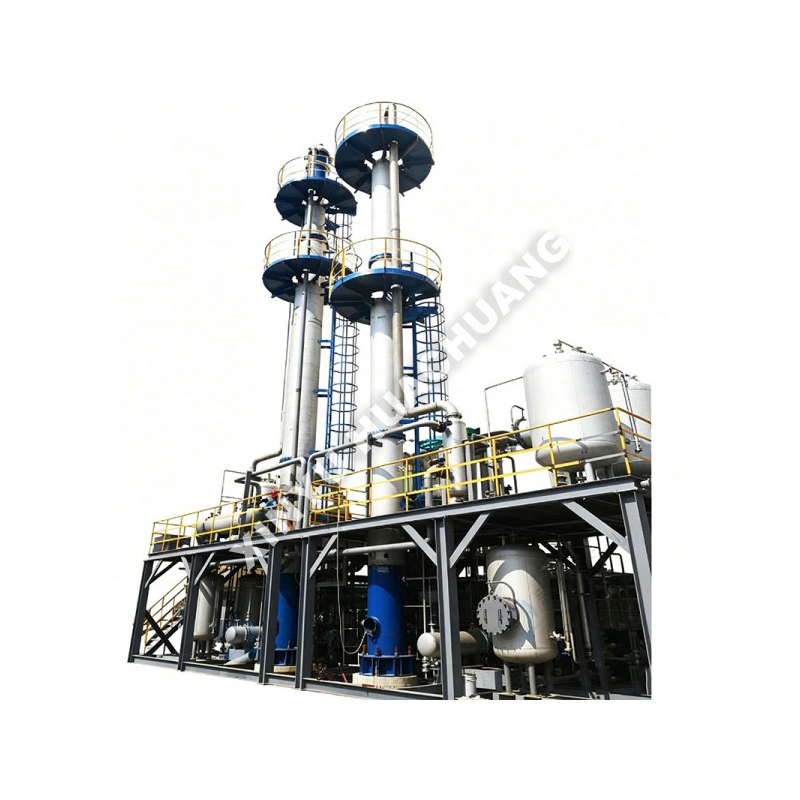
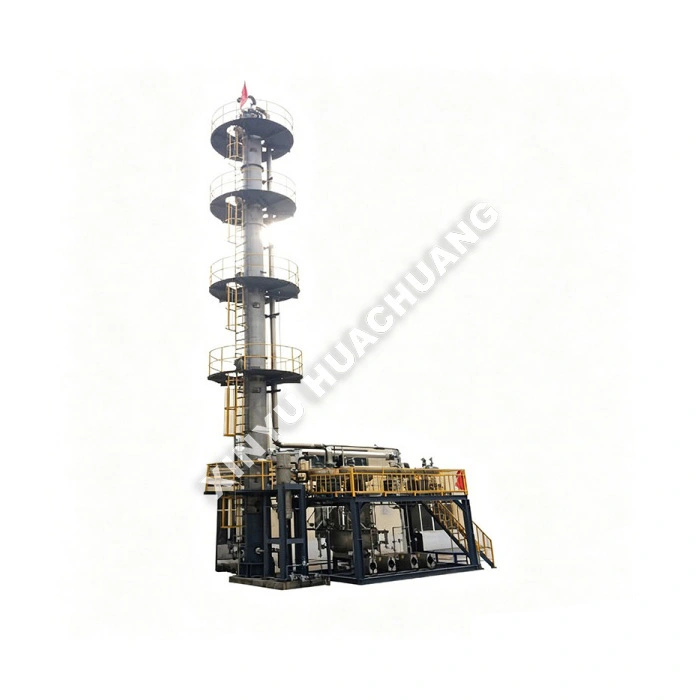
Methanol Recovery Distillation Unit
  • Methanol Recovery Distillation UnitMethanol Recovery Distillation Unit
  • Methanol Recovery Distillation UnitMethanol Recovery Distillation Unit
  • Methanol Recovery Distillation UnitMethanol Recovery Distillation Unit

Methanol Recovery Distillation Unit

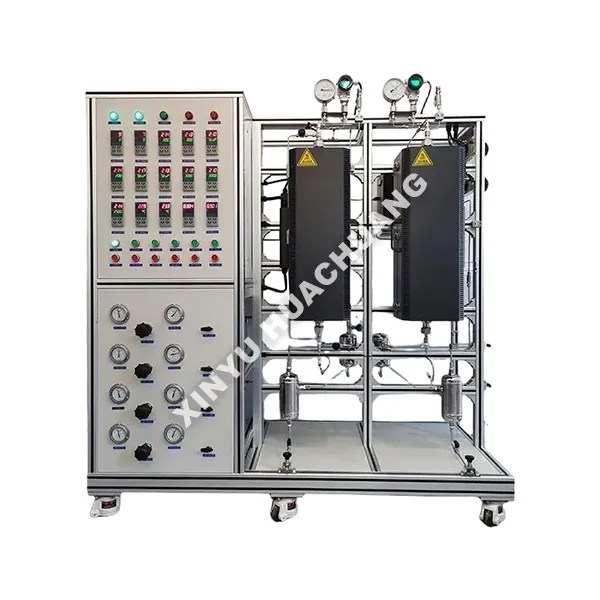
Recovering methanol from waste water streams with energy efficiency and consistent purity? XINYU HUACHUANG, as a professional chemical equipment manufacturer, designs its Methanol Recovery Distillation Unit for continuous fractional distillation with SS304/SS316L construction (Hastelloy or 904L optional). Integrated with preheaters, vacuum systems, and GC for real time purity monitoring. Top product meets spec; bottoms discharged. Ask for a customized solution with your typical feed composition and capacity.

The XINYU HUACHUANG Methanol Recovery Distillation Unit is a highly efficient, continuous separation system specifically engineered for the industrial recovery of methanol from aqueous waste streams and mixed solvents. Designed to maximize energy efficiency and product throughput, this unit utilizes advanced multi-column configurations and heat integration technologies to separate complex mixtures with exceptional precision. Equipped with intelligent PLC automation, automated reflux ratio control, and multi-level safety interlocks, the Methanol Recovery Distillation Unit ensures stable, unattended long-term operation while delivering ultra-high purity recovered methanol (≥99.9%) for commercial reuse and process optimization.

Methanol Recovery Distillation Unit

Working Principle

● Core Mechanism: The unit operates on a continuous fractional distillation principle. The waste methanol-water mixture is continuously fed into the system and preheated before entering the primary column. As the mixture is heated in the reboiler, vapor rises through the column internals, undergoing repeated condensation and revaporization. Methanol (boiling point ~64.7°C) is continuously drawn from the top condenser as the purified product, while water and heavier impurities are discharged from the bottom. This continuous cascade across multiple columns allows for the precise separation of complex mixtures into high-purity fractions.

● Reactor Materials: To ensure durability, corrosion resistance, and product purity, the entire system is constructed from premium stainless steel. Standard SS304/316L is used for most applications, while highly corrosive environments or high-purity pharmaceutical requirements may utilize specialized alloys like Hastelloy or 904L.

● Process Integration: This versatile Methanol Recovery Distillation Unit pairs seamlessly with various upstream and downstream processes. It integrates flawlessly with preheaters, vacuum systems for heat-sensitive materials, automated product fraction collectors, and online analytical instruments (e.g., GC) for real-time purity monitoring and automated cut-point adjustment.

Technical Specifications

Parameter

Specification

System Configuration

Multi-Column Continuous Fractionation (Customizable stages)

Operating Temperature

RT ~ 150℃ (Precision ±1℃)

Operating Pressure

Atmospheric / Deep Vacuum / Slight Positive Pressure

Heating Method

Steam Jacket / Thermal Oil / Electric Heating

Column Internals

Structured Packing / Random Packing / Sieve Trays

Reflux Ratio

Fully Automatic Adjustable (1:1 to 99:1)

Control System

Industrial PLC + PC Software Interface

System Material

SS304 / SS316L / Hastelloy (Customizable)

How to Choose Right?

● Define Your Feedstock & Target Products: Clearly identify the composition of your waste stream (e.g., methanol-water ratio, presence of other solvents) and required product purity. This determines the number of columns, column heights, and internal configurations needed for the Methanol Recovery Distillation Unit.

● Material Compatibility: Select the appropriate stainless steel grade based on the chemical properties of your mixture. Standard SS316L is suitable for most organic solvents, while highly corrosive acids or bases require Hastelloy or specialized cladding.

● Capacity & Throughput: Determine your required continuous processing volume (e.g., L/h or kg/h). Ensure the column diameter and reboiler capacity are correctly sized to handle the vapor velocity without flooding.

● Thermal Sensitivity: If processing heat-sensitive materials, opt for a vacuum system configuration to lower the boiling points and prevent thermal degradation.

Product Comparison

Feature

Single-Column / Batch Unit

XINYU HUACHUANG Methanol Recovery Distillation Unit

Operation Mode

Intermittent / Batch

True Continuous Processing

Separation Capacity

Limited to binary/simple mixtures

Multi-component complex mixture separation

Energy Efficiency

Lower (Repeated heating/cooling cycles)

High (Heat integration & continuous steady state)

Product Consistency

Varies by batch

Highly consistent, automated cut-points

Labor Requirement

High manual intervention

Fully automated, unattended operation

Why Choose Us

● Direct Factory Pricing: As the original manufacturer, we eliminate middlemen, offering highly competitive pricing without compromising on industrial-grade quality.

● Deep Customization Capability: From column internals to control logic, our engineering team tailors every detail to your specific continuous separation research and production needs.

● Industrial-Grade Reliability: Built with top-tier components (e.g., premium pumps, industrial PLCs, high-efficiency condensers) and rigorous factory testing, ensuring long-term stability for 24/7 continuous operation.

● Comprehensive After-Sales Support: We provide lifetime technical support, English video tutorials, and remote troubleshooting via video calls to ensure your production never stops.

● ISO-Certified Quality: Every unit undergoes strict pressure testing, leak detection, and temperature uniformity calibration before shipment, backed by our ISO quality management system.

After-Sales Service & Support

At XINYU HUACHUANG, we are committed to providing comprehensive and reliable after-sales support to ensure the continuous and efficient operation of your equipment. Our dedicated service team is always ready to assist you.

Comprehensive Warranty Coverage

We proudly offer a two-year warranty for our equipment. During this period, we provide free maintenance and repair services for any quality-related issues, excluding those caused by improper operation, unauthorized modifications, or force majeure. For equipment beyond the two-year warranty period, we continue to offer lifelong maintenance services, charging only the cost of replacement parts and labor.

Rapid Response Mechanism

We offer 7×24 hours professional engineering telephone support. Upon receiving a fault notification, our technical team will respond within 24 hours and provide a viable solution. If on-site service is required, our professional engineers will arrive at your facility within one week. In special circumstances where the equipment cannot be repaired, we will unconditionally replace it with a new unit or provide a substitute unit during the two-year warranty period, or take necessary measures to restore normal operation.

Frequently Asked Questions (FAQ)

Q1: What types of waste methanol streams can this unit recover?

A: The unit handles a wide range of waste methanol-water mixtures from pharmaceutical synthesis, chemical manufacturing, electronic cleaning, and solvent washing processes. Whether the waste stream contains 10% or 90% methanol, the continuous multi-column cascade can separate and recover high-purity methanol for direct reuse or resale.

Q2: How does the continuous cascade design improve recovery efficiency compared to single-column systems?

A: The primary column performs the bulk separation, concentrating methanol overhead while discharging water-rich bottoms. Additional columns provide further purification passes, stripping residual water and heavy impurities to achieve product purities that a single column cannot reach. This staged approach maximizes both recovery yield and final product quality.

Q3: What construction materials are used, and how do they protect against methanol-induced corrosion?

A:The entire system is made of high-quality stainless steel. The standard SS304/316L is suitable for most applications and offers excellent resistance to methanol corrosion. For harsh corrosive environments or high-purity pharmaceutical requirements, special alloys such as Hastelloy or 904L can be selected to ensure the long lifespan of the equipment and product integrity.

Q4: How does the unit support real-time quality control during recovery operations?

A: It integrates flawlessly with online analytical instruments such as GC for real-time purity monitoring of the recovered methanol stream. Automated cut-point adjustment ensures that only on-spec material is collected as product, while off-spec fractions are automatically diverted back for reprocessing—no manual intervention required.

Q5: Can this unit be integrated with existing plant processes for solvent recovery?

A: Yes. The Methanol Recovery Distillation Unit pairs seamlessly with upstream preheaters and downstream automated product fraction collectors. It can also be connected to vacuum systems for processing heat-sensitive mixtures and to plant-wide DCS/SCADA systems for centralized monitoring and control, making it a true plug-and-play addition to existing facilities.


Send Inquiry
Contact Info
  • Address

    Unit 104, Building A, Factory D8 (East Zone), No. 1 Xuefu West Road, Xuefu Industrial Zone, Xiqing District, Tianjin, Hebei Province, China

Tell XINYU HUACHUANG your reaction type, temperature, pressure and analytical needs, and our team will reply within 24 hours with a tailored quote.
X
We use cookies to offer you a better browsing experience, analyze site traffic and personalize content. By using this site, you agree to our use of cookies. Privacy Policy
RejectAccept