Products
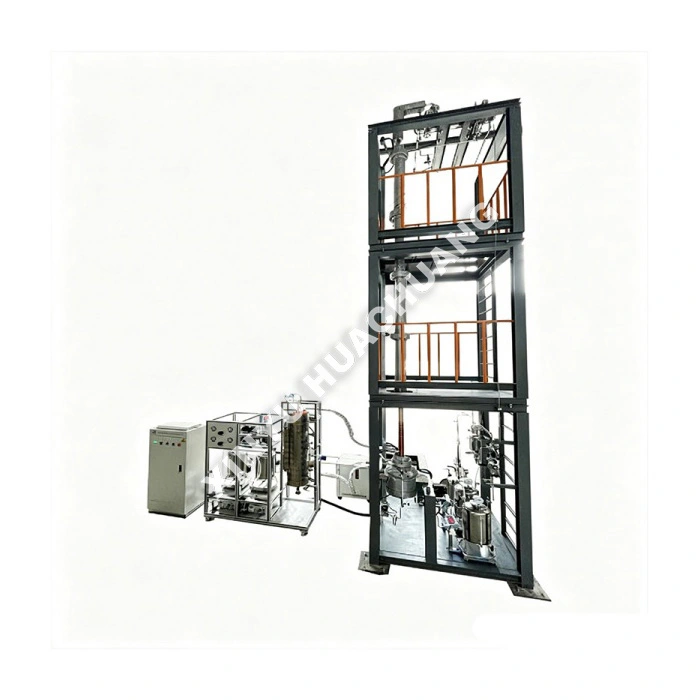
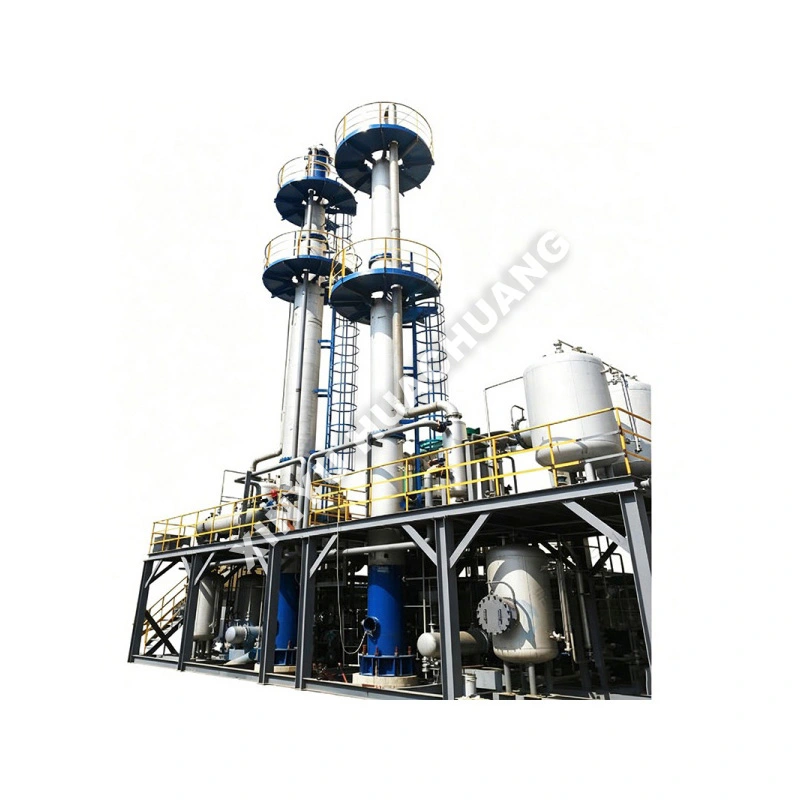
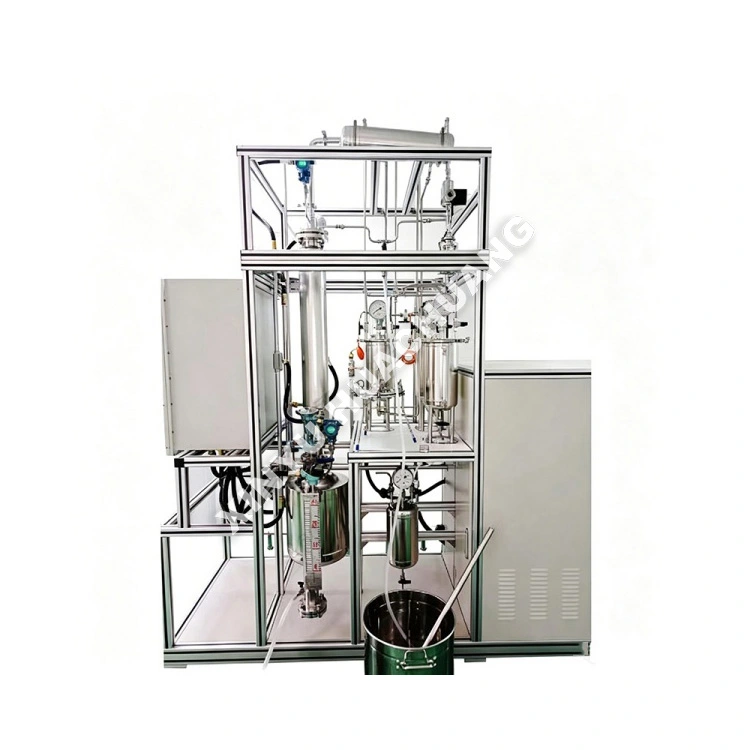
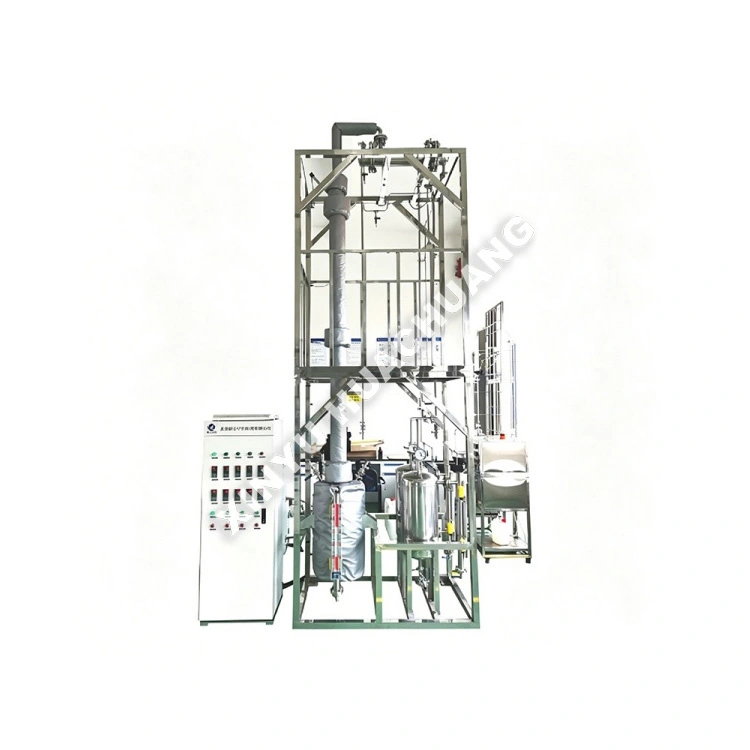
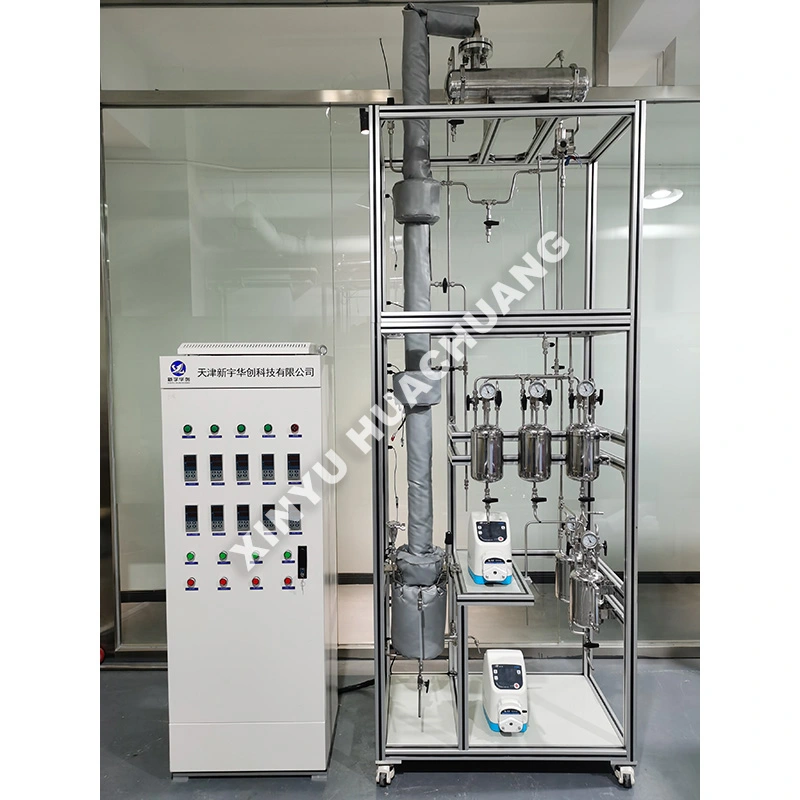
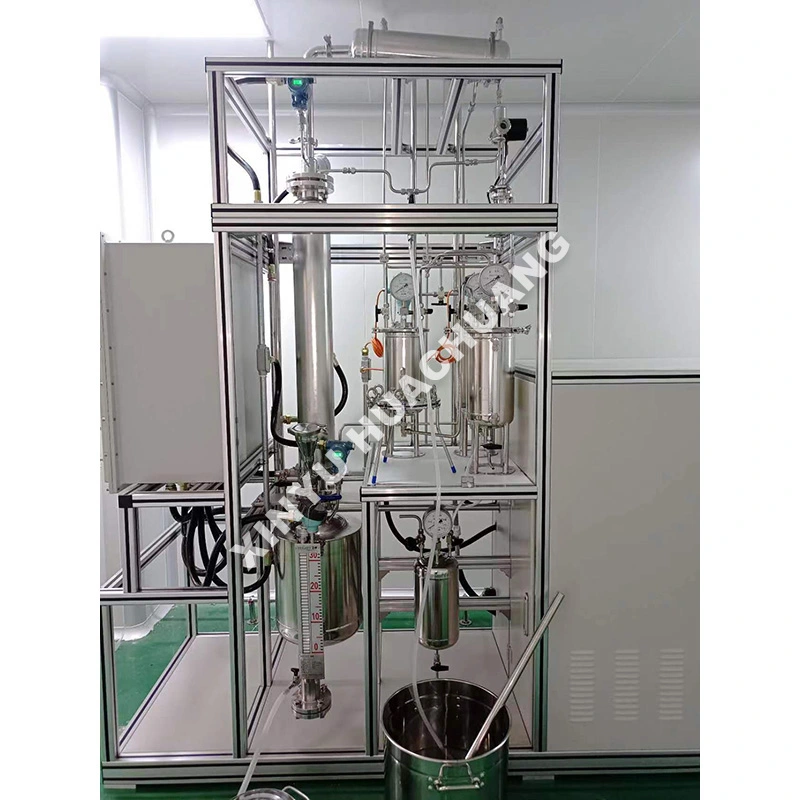
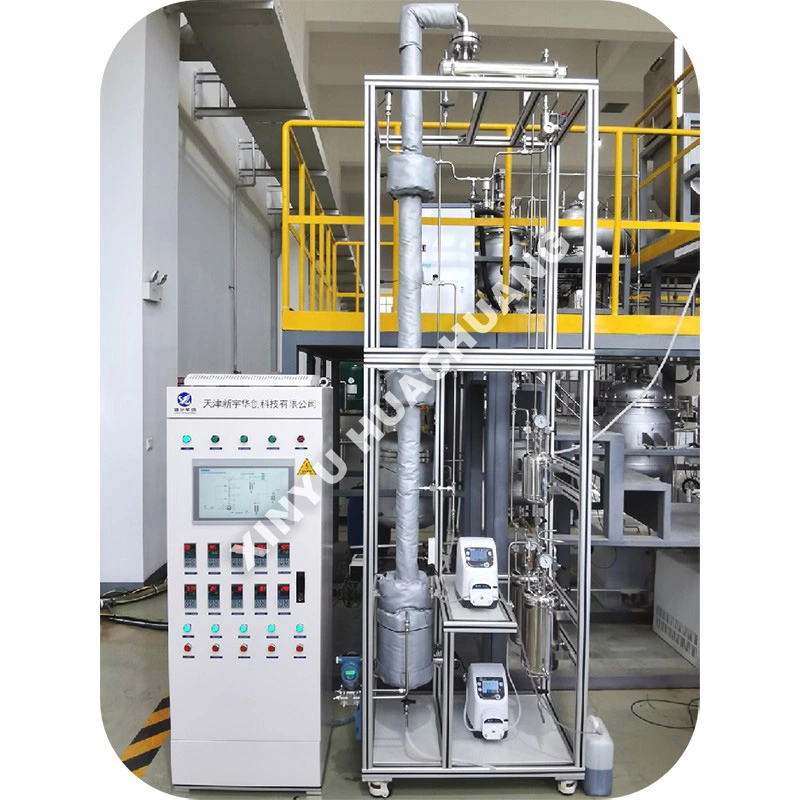
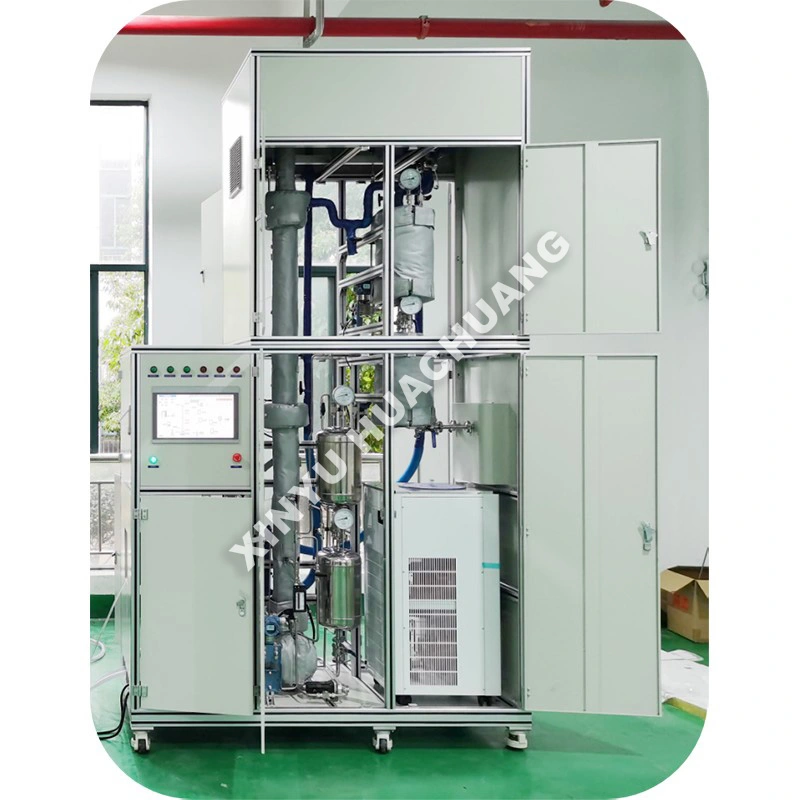
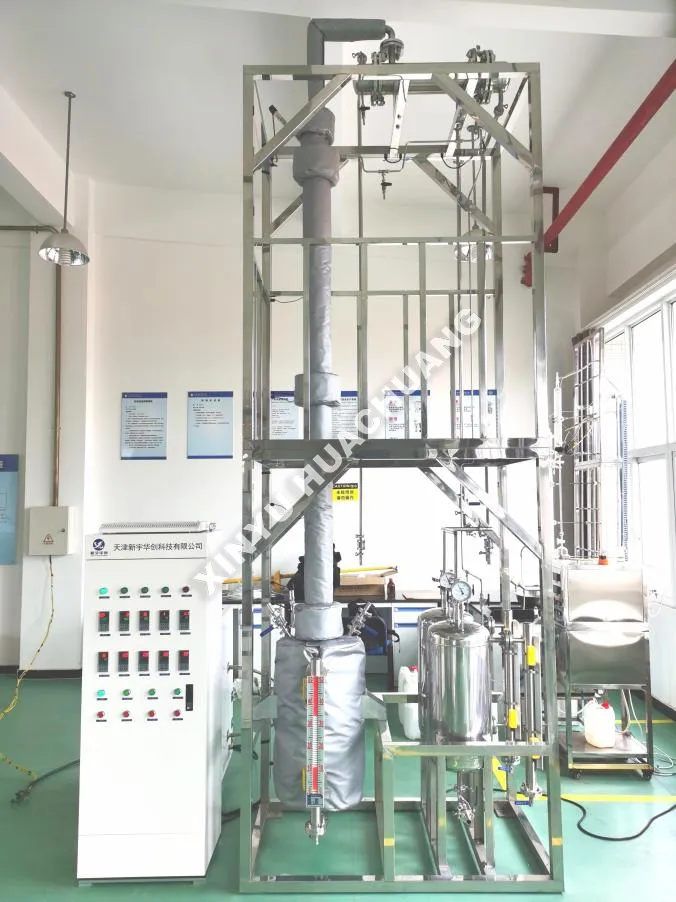
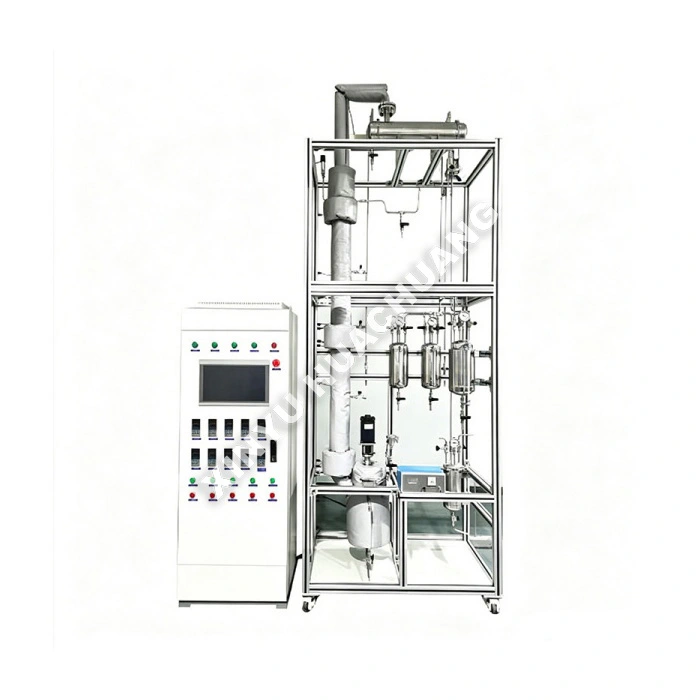
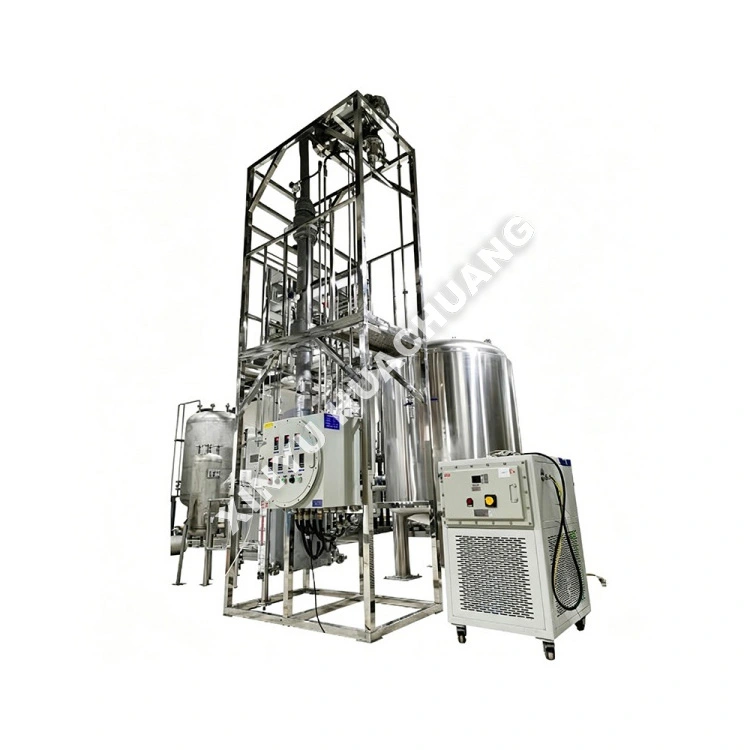
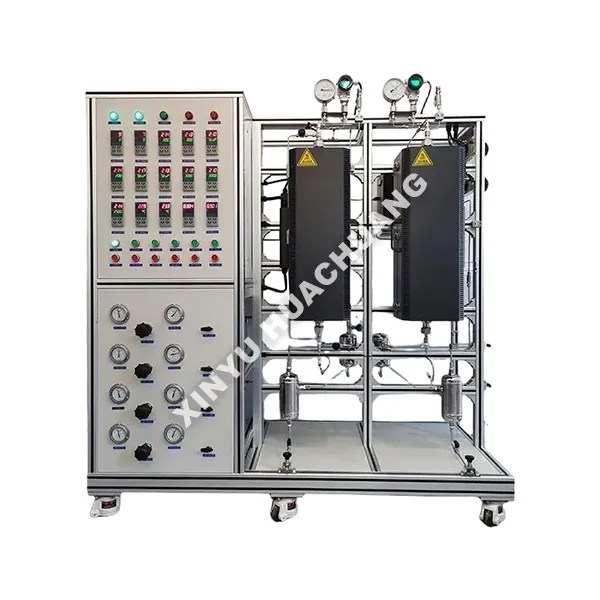
50L Batch Distillation Unit
  • 50L Batch Distillation Unit50L Batch Distillation Unit
  • 50L Batch Distillation Unit50L Batch Distillation Unit
  • 50L Batch Distillation Unit50L Batch Distillation Unit
  • 50L Batch Distillation Unit50L Batch Distillation Unit
  • 50L Batch Distillation Unit50L Batch Distillation Unit

50L Batch Distillation Unit

Pilot scale solvent recovery or essential oil purification? XINYU HUACHUANG specializes in R&D and manufacturing of chemical separation equipment. Its 50L Batch Distillation Unit gives you a full fractionating column on a manageable batch scale, covering heating, reflux, and collection. Yield and purity data you can trust for scale up. Easy to operate and clean. Contact us for a quote today.

The XINYU HUACHUANG 50L Batch Distillation Unit is a highly efficient, pilot-scale separation system specifically engineered for medium-volume purification and solvent recovery applications. Designed to bridge the gap between benchtop laboratory research and industrial mass production, this unit accurately controls reflux ratios, heating temperatures, and distillation rates. Equipped with intelligent PLC automation and multi-level safety interlocks, the 50L Batch Distillation Unit ensures safe, unattended long-term operation while delivering highly reproducible purity data for process optimization and scale-up.

50L Batch Distillation Unit

What is a 50L Batch Distillation Unit?

A 50L Batch Distillation Unit is a specialized chemical separation apparatus designed to process medium-sized batches of liquid mixtures. It operates by heating the mixture in a 50-liter reactor to vaporize the more volatile components, which then travel up a fractionating column. The vapor undergoes repeated condensation and revaporization to achieve high-purity separation. This unit is widely utilized for pilot-scale solvent recovery, essential oil extraction, fine chemical purification, and pharmaceutical intermediate processing, providing reliable yield and purity metrics before full-scale industrial implementation.

What are the distinctive advantages?

● Pilot-Scale Capacity: The 50L reactor volume is ideal for pilot-scale testing, providing sufficient product yield for downstream analysis while saving raw material costs compared to industrial units.

● High-Precision Separation: Features an adjustable reflux ratio system and multi-zone temperature control to achieve high-purity fractions and minimize product loss.

● Intelligent PLC Automation: Centralized control system enables unattended long-term operation, automated data logging (temperature, pressure, flow), and historical curve generation.

● Robust & Safe Construction: Built with premium metallurgy (e.g., SS316L, Glass-lined) and multi-level safety interlocks (over-temperature, over-pressure, dry-heating protection) to ensure safe operation.

● Energy-Efficient Design: Optimized heating jackets and high-efficiency condensers maximize heat transfer and solvent recovery rates, reducing overall operational costs.

Technical Specifications

Parameter

Specification

Reactor Volume

50L (Customizable)

Operating Temperature

RT ~ 300℃ (Precision ±1℃)

Operating Pressure

Atmospheric / Vacuum / Slight Positive Pressure

Heating Method

Electric Heating Jacket / Oil Bath / Steam

Column Type

Packed Column / Plate Column / Spinning Band

Reflux Ratio

Adjustable (Manual or Automatic)

Control System

Industrial PLC + PC Software Interface

Reactor Material

SS316L / Glass-lined / Hastelloy (Customizable)

Where is it applicable?

● Fine Chemicals & Pharmaceuticals: Pilot-scale purification of active pharmaceutical ingredients (APIs) and high-value chemical intermediates.

● Solvent Recovery: Efficient recovery and purification of waste solvents (e.g., ethanol, acetone, toluene) for reuse in production.

● Essential Oils & Extracts: Gentle distillation of plant extracts, terpenes, and natural fragrances to preserve active compounds.

● Food & Beverage: Concentration of fruit juices, alcohol purification, and flavor essence extraction.

● Process R&D: Gathering reliable kinetic and separation data for industrial continuous distillation scale-up.

From Concept to Crate: Our End-to-End Build Cycle

1. Requirement Confirmation: Understand the client's specific feedstock properties, target purity, and operating parameters to customize the technical proposal.

2. Design & Engineering: Finalize CAD drawings, P&ID diagrams, and electrical schematics for the 50L distillation system.

3. Precision Manufacturing: Fabrication of the 50L reactor vessel, fractionating column, condenser, and PLC control cabinet.

4. Factory Testing: Strict pressure/vacuum testing, temperature uniformity calibration, and comprehensive PLC logic debugging.

5. Packaging & Shipping: Export-standard fumigation-free wooden crate packaging with secure internal fixation for global logistics.

6. Installation & Support: Provide comprehensive English manuals, video installation guides, and free online technical support for seamless operation.

After-Sales Service & Support

At XINYU HUACHUANG, we are committed to providing comprehensive and reliable after-sales support to ensure the continuous and efficient operation of your equipment. Our dedicated service team is always ready to assist you.

Comprehensive Warranty Coverage

We proudly offer a two-year warranty for our equipment. During this period, we provide free maintenance and repair services for any quality-related issues, excluding those caused by improper operation, unauthorized modifications, or force majeure. For equipment beyond the two-year warranty period, we continue to offer lifelong maintenance services, charging only the cost of replacement parts and labor.

Rapid Response Mechanism

We offer 7×24 hours professional engineering telephone support. Upon receiving a fault notification, our technical team will respond within 24 hours and provide a viable solution. If on-site service is required, our professional engineers will arrive at your facility within one week. In special circumstances where the equipment cannot be repaired, we will unconditionally replace it with a new unit or provide a substitute unit during the two-year warranty period, or take necessary measures to restore normal operation.

Frequently Asked Questions (FAQ)

Q1: What batch size is the 50L Batch Distillation Unit designed for?

A: With a 50-liter reactor, the unit is designed to process medium-sized batches of liquid mixtures, bridging the gap between small lab glassware and full industrial columns.

Q2: How does the unit achieve high-purity separation?

A: The mixture is heated in the reactor to vaporize the more volatile components, which travel up the fractionating column. The vapor undergoes repeated condensation and revaporization inside the column, progressively boosting purity.

Q3: What are the typical applications of this unit?

A: It is widely utilized for pilot-scale solvent recovery, essential oil extraction, fine chemical purification, and pharmaceutical intermediate processing.

Q4: Can this unit provide data for industrial scale-up?

A: Yes. The unit delivers reliable yield and purity metrics at medium batch scale, allowing you to verify separation performance before full-scale industrial implementation.

Q5: When should we choose this batch unit instead of a continuous system?

A: Batch operation processes one batch at a time, offering the flexibility to switch feedstocks and products easily. For medium-sized batches and pilot-scale trials, this 50L unit is often the more practical choice.


Send Inquiry
Contact Info
  • Address

    Unit 104, Building A, Factory D8 (East Zone), No. 1 Xuefu West Road, Xuefu Industrial Zone, Xiqing District, Tianjin, Hebei Province, China

Tell XINYU HUACHUANG your reaction type, temperature, pressure and analytical needs, and our team will reply within 24 hours with a tailored quote.
X
We use cookies to offer you a better browsing experience, analyze site traffic and personalize content. By using this site, you agree to our use of cookies. Privacy Policy
RejectAccept