Products
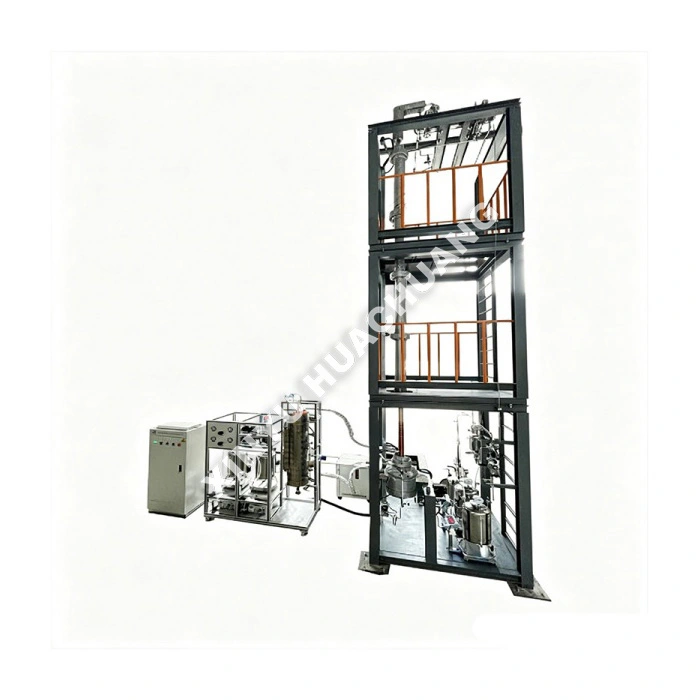
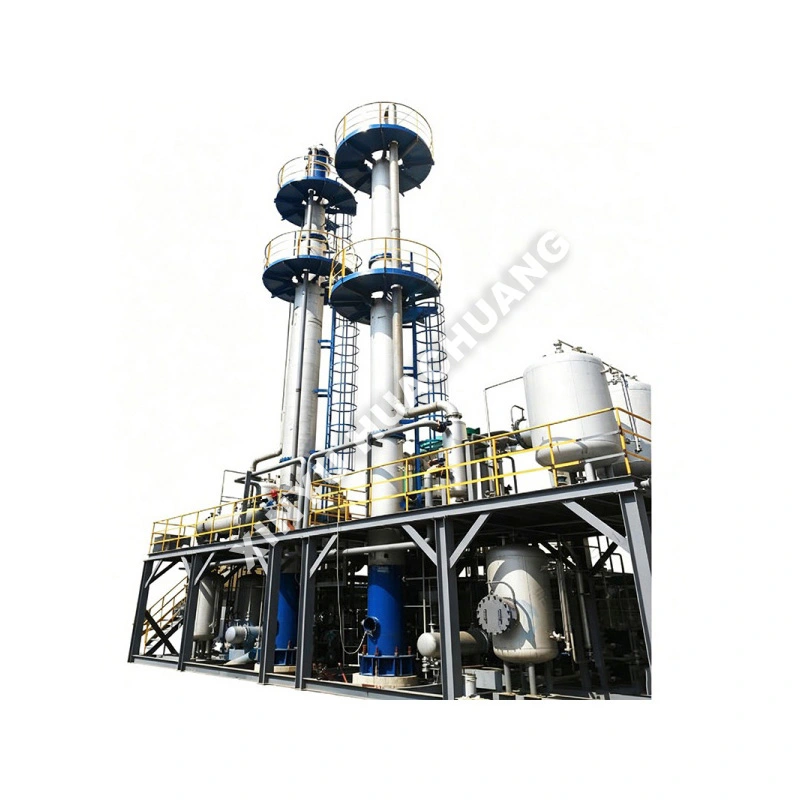
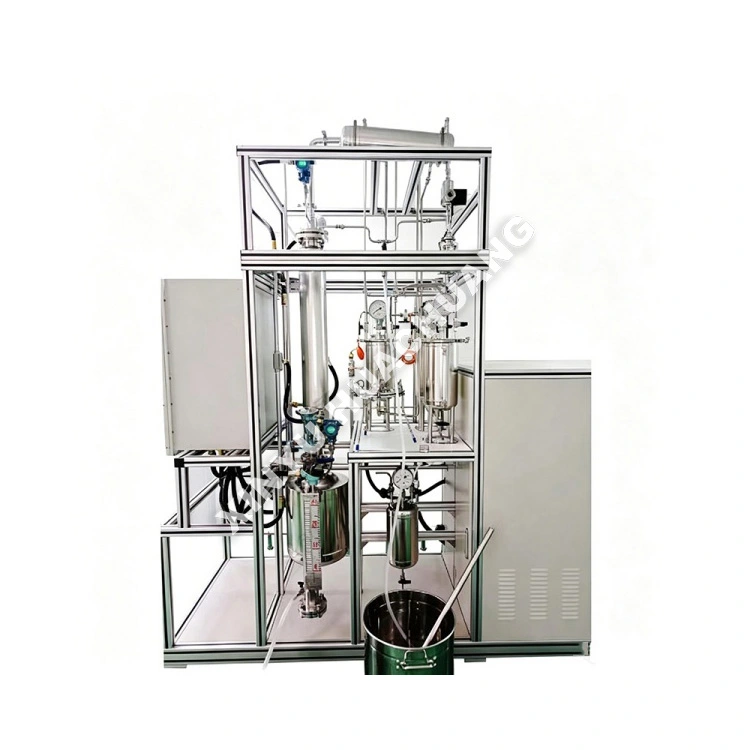
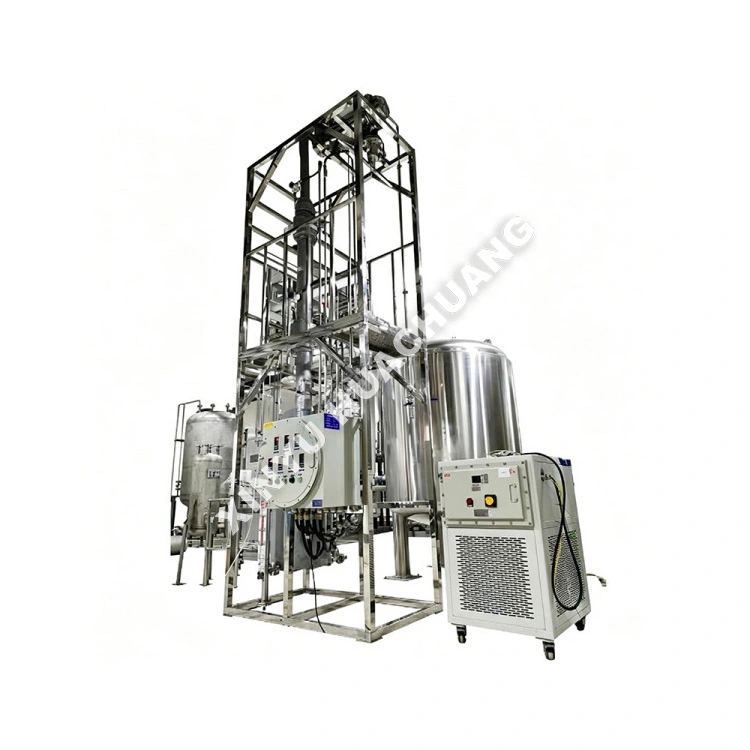
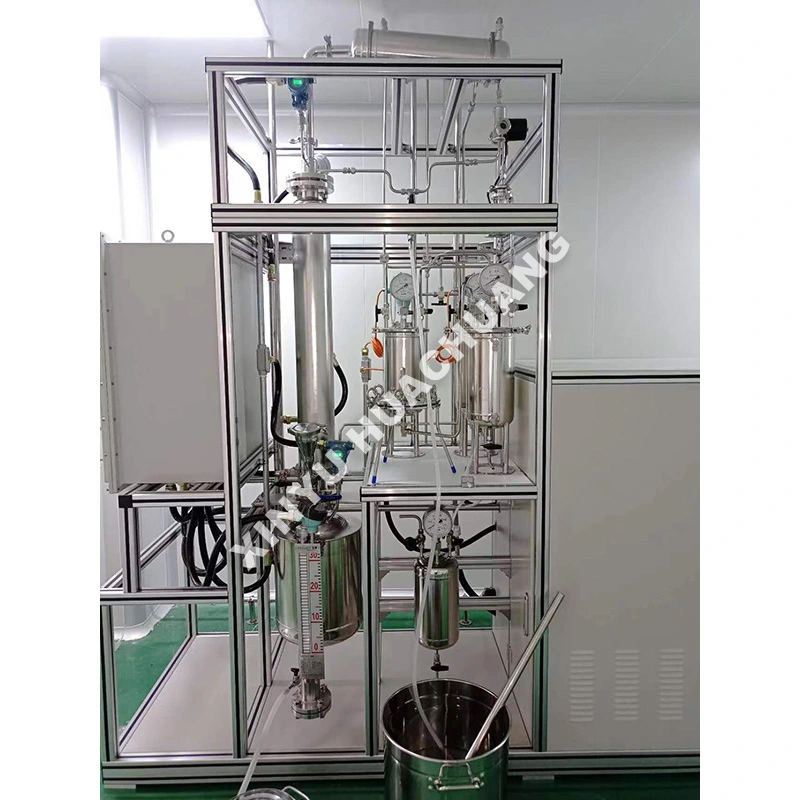
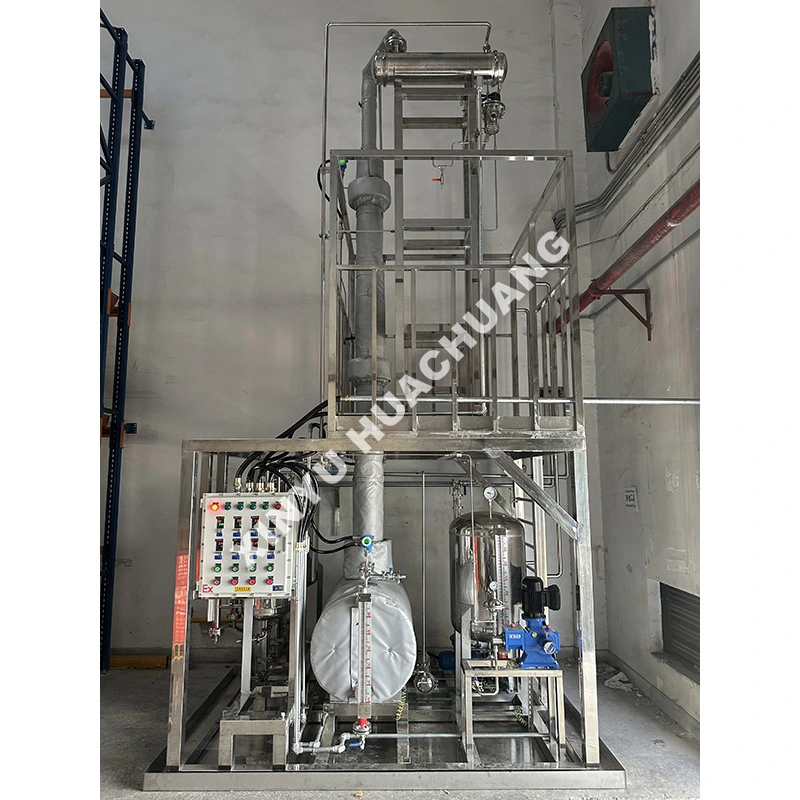
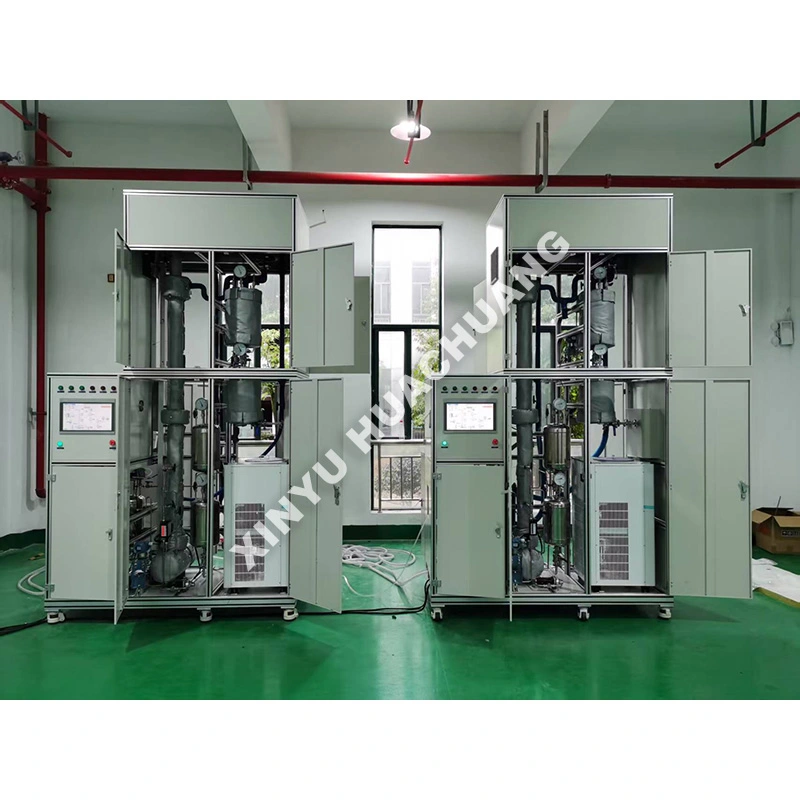
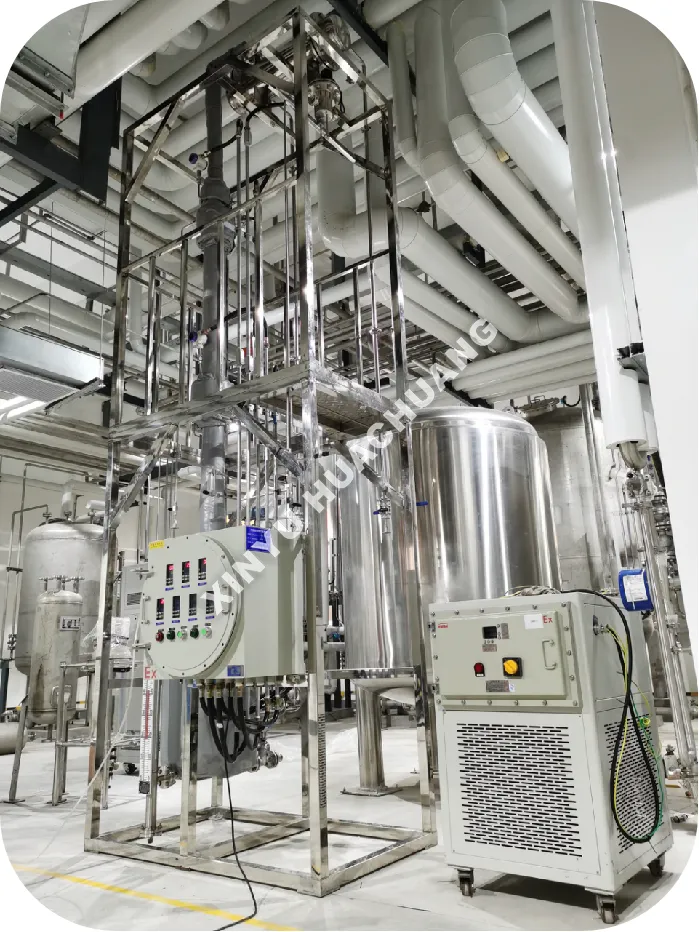
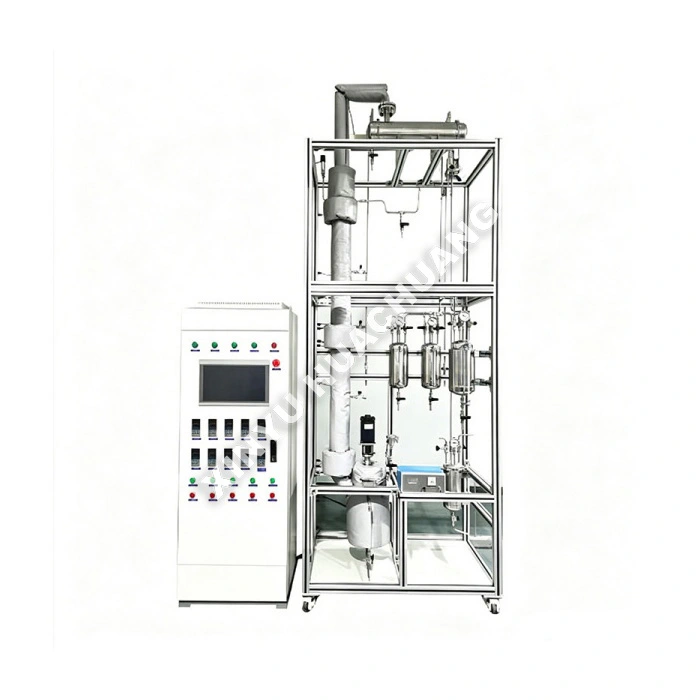
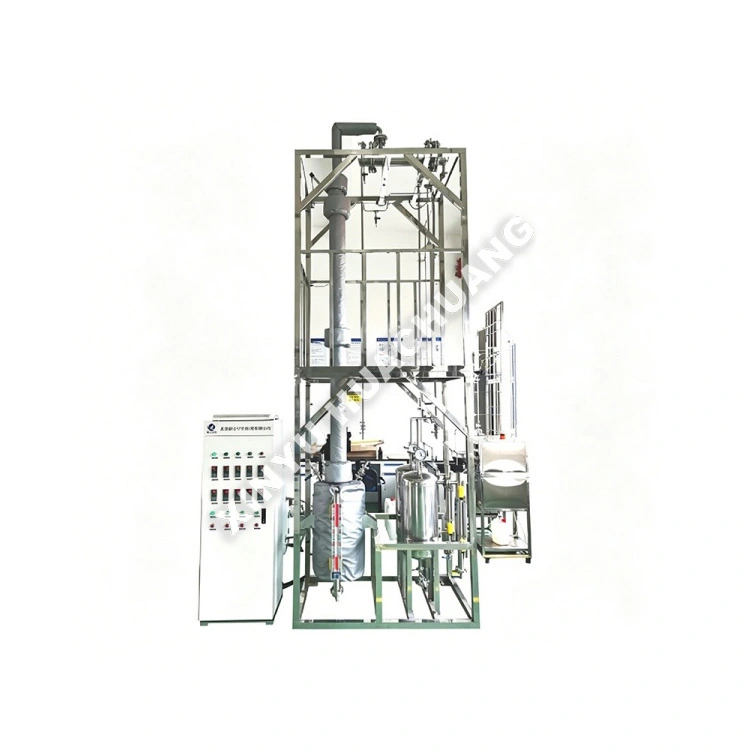
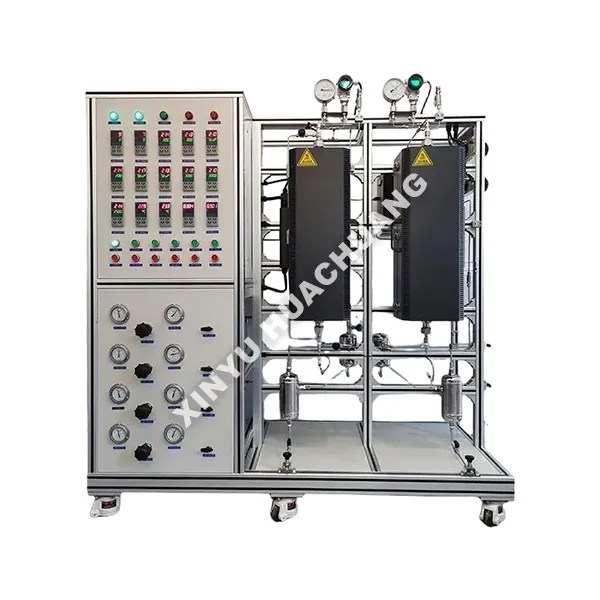
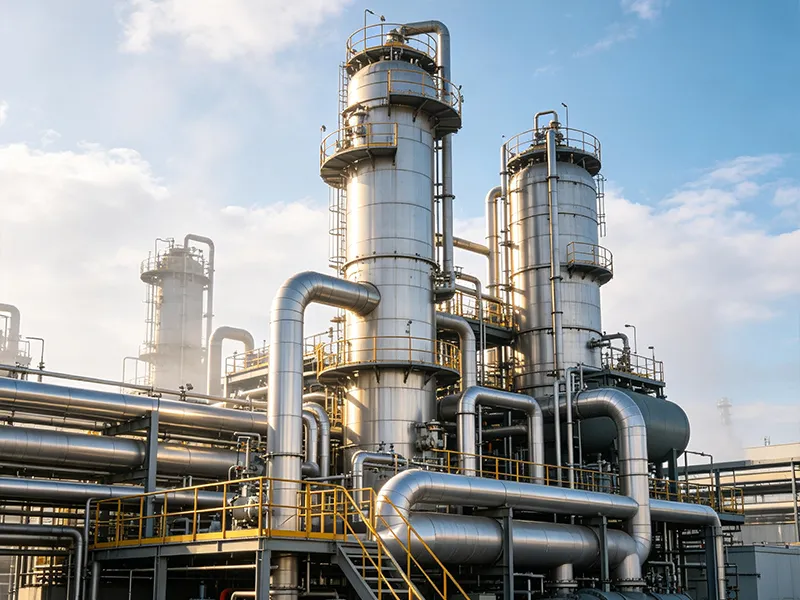
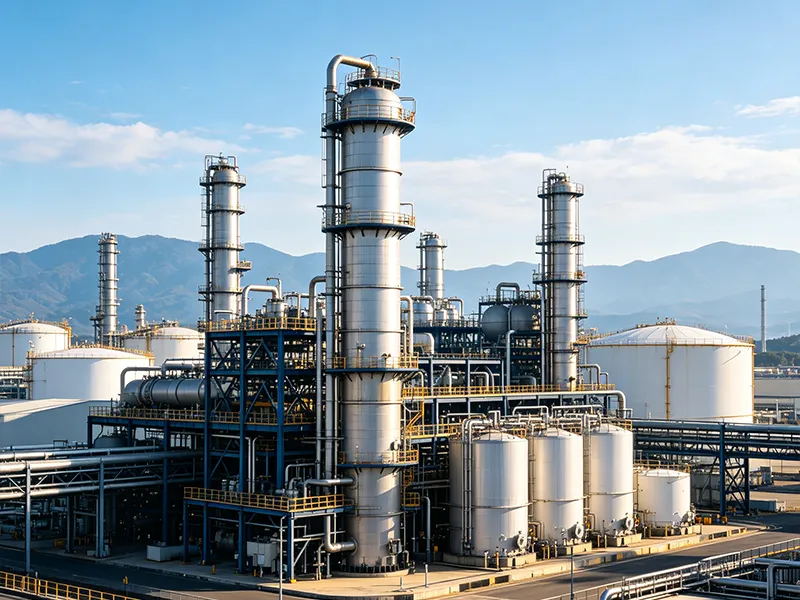
60L Explosion-Proof Batch Distillation Unit
  • 60L Explosion-Proof Batch Distillation Unit60L Explosion-Proof Batch Distillation Unit
  • 60L Explosion-Proof Batch Distillation Unit60L Explosion-Proof Batch Distillation Unit
  • 60L Explosion-Proof Batch Distillation Unit60L Explosion-Proof Batch Distillation Unit
  • 60L Explosion-Proof Batch Distillation Unit60L Explosion-Proof Batch Distillation Unit

60L Explosion-Proof Batch Distillation Unit

Distilling flammable solvents? Safety comes first. XINYU HUACHUANG's 60L Explosion-Proof Batch Distillation Unit features Exd and Exe certified motors, heating jackets, and control cabinets, isolating every ignition source from hazardous vapors. As a professional manufacturer, we know compliance matters. Same capacity, same separation power, but built for environments where standard units do not belong. Get your full ATEX and IECEx compliance quote.

The XINYU HUACHUANG 60L Explosion-Proof Batch Distillation Unit is a highly specialized pilot-scale separation system engineered specifically for processing flammable and volatile organic solvents. Designed to bridge the gap between laboratory R&D and industrial mass production, this unit accurately controls reflux ratios, heating temperatures, and distillation rates within a strictly safe environment. Equipped with certified explosion-proof electrical components, intelligent PLC automation, and multi-level safety interlocks, the 60L Explosion-Proof Batch Distillation Unit ensures unattended long-term operation while delivering highly reproducible purity data for process optimization and scale-up.

60l Explosion Proof Batch Distillation Unit

What is a 60L Explosion-Proof Batch Distillation Unit?

A 60L Explosion-Proof Batch Distillation Unit is a specialized chemical separation apparatus designed to safely process medium-sized batches of hazardous, flammable liquid mixtures. It operates by heating the mixture in a 60-liter reactor to vaporize the more volatile components, which then travel up a fractionating column for high-purity separation. The defining feature of this unit is its comprehensive explosion-proof design, including Exd/Exe certified motors, heating jackets, and control cabinets, which completely isolate potential ignition sources from the hazardous atmosphere. This unit is widely utilized for pilot-scale solvent recovery, fine chemical purification, and pharmaceutical intermediate processing, providing reliable yield and purity metrics before full-scale industrial implementation.

What are the distinctive advantages?

● Certified Explosion-Proof Safety: All electrical components, including stirrer motors, heating systems, and control panels, are strictly certified (e.g., Exd IIB/IIC T4/T6) to prevent sparks and ensure safe operation in hazardous environments.

● Pilot-Scale Capacity: The 60L reactor volume is ideal for pilot-scale testing, providing sufficient product yield for downstream analysis while saving raw material costs compared to industrial units.

● High-Precision Separation: Features an adjustable reflux ratio system and multi-zone temperature control to achieve high-purity fractions and minimize product loss.

● Intelligent PLC Automation: Centralized control system enables unattended long-term operation, automated data logging (temperature, pressure, flow), and historical curve generation.

● Robust & Safe Construction: Built with premium metallurgy (e.g., SS316L, Glass-lined) and multi-level safety interlocks (over-temperature, over-pressure, dry-heating protection) to ensure safe operation.

Technical Specifications

Parameter

Specification

Reactor Volume

60L (Customizable)

Operating Temperature

RT ~ 300℃ (Precision ±1℃)

Operating Pressure

Atmospheric / Vacuum / Slight Positive Pressure

Heating Method

Explosion-Proof Electric Heating Jacket / Oil Bath

Column Type

Packed Column / Plate Column / Spinning Band

Reflux Ratio

Adjustable (Manual or Automatic)

Control System

Industrial PLC + PC Software Interface

Explosion-Proof Rating

Exd IIB/IIC T4/T6 (Customizable per zone)

Reactor Material

SS316L / Glass-lined / Hastelloy (Customizable)

How to Match Your Testing Requirements with Our Unit

● Hazardous Area Classification: Determine the specific explosive gas mixture (e.g., Group IIA, IIB, or IIC) and temperature class (T1-T6) in your facility to select the correct explosion-proof rating for the 60L Explosion-Proof Batch Distillation Unit.

● Feedstock Compatibility: Select the appropriate reactor material based on the chemical properties of your mixture. Standard SS316L is suitable for most applications, while highly corrosive environments require glass-lined or Hastelloy reactors.

● Separation Difficulty: Evaluate the boiling point difference of your mixture. For close-boiling components, opt for a high-efficiency packed column or spinning band column to maximize separation efficiency.

● Vacuum Requirements: If processing heat-sensitive materials, ensure the unit is equipped with a high-performance vacuum system and mechanical seals designed for continuous low-pressure operation.

Quality Inspection Process

● Material Verification: Strict inspection of incoming stainless steel and explosion-proof electrical components to ensure they meet specified metallurgical standards and safety certifications.

● Precision Machining: CNC machining of the 60L reactor body and flanges to guarantee perfect sealing surfaces and structural integrity under vacuum or pressure.

● Hydrostatic/Vacuum Test: Every reactor undergoes rigorous hydrostatic pressure testing and vacuum leak testing to verify structural safety and leak-proof performance.

● Explosion-Proof Inspection: Comprehensive testing of all electrical wiring, grounding connections, and motor enclosures to ensure strict compliance with explosion-proof safety standards.

● Final Functional Run: A complete dry-run test of the heating, stirring, and PLC control systems to verify smooth operation, uniform thermal distribution, and proper functioning of safety interlocks before packaging.

After-Sales Service & Support

At XINYU HUACHUANG, we are committed to providing comprehensive and reliable after-sales support to ensure the continuous and efficient operation of your equipment. Our dedicated service team is always ready to assist you.

Comprehensive Warranty Coverage

We proudly offer a two-year warranty for our equipment. During this period, we provide free maintenance and repair services for any quality-related issues, excluding those caused by improper operation, unauthorized modifications, or force majeure. For equipment beyond the two-year warranty period, we continue to offer lifelong maintenance services, charging only the cost of replacement parts and labor.

Rapid Response Mechanism

We offer 7×24 hours professional engineering telephone support. Upon receiving a fault notification, our technical team will respond within 24 hours and provide a viable solution. If on-site service is required, our professional engineers will arrive at your facility within one week. In special circumstances where the equipment cannot be repaired, we will unconditionally replace it with a new unit or provide a substitute unit during the two-year warranty period, or take necessary measures to restore normal operation.

Frequently Asked Questions (FAQ)

Q1: What makes this unit suitable for flammable and hazardous liquid mixtures?

A: The 60L Explosion-Proof Batch Distillation Unit is built with a comprehensive explosion-proof design that completely isolates potential ignition sources from the hazardous atmosphere, making it safe for processing medium-sized batches of flammable liquids.

Q2: Which components carry explosion-proof certification?

A: The motors, heating jackets, and control cabinets are all Exd/Exe certified, covering the main electrical and heating elements of the system with recognized explosion protection.

Q3: How does the explosion-proof design isolate ignition sources?

A: By using Exd/Exe certified motors, heating jackets, and control cabinets, the design keeps electrical sparks and hot surfaces from contacting the hazardous atmosphere around the unit.

Q4: What applications is the 60L explosion-proof unit commonly used for?

A: It is widely utilized for pilot-scale solvent recovery, fine chemical purification, and pharmaceutical intermediate processing where flammable solvents are involved.

Q5: Does the explosion-proof design affect separation performance?

A: No. The unit keeps the same working principle—heating the mixture in a 60-liter reactor and separating the more volatile components in a fractionating column for high-purity results, with reliable yield and purity metrics before scale-up.


Send Inquiry
Contact Info
  • Address

    Unit 104, Building A, Factory D8 (East Zone), No. 1 Xuefu West Road, Xuefu Industrial Zone, Xiqing District, Tianjin, Hebei Province, China

Tell XINYU HUACHUANG your reaction type, temperature, pressure and analytical needs, and our team will reply within 24 hours with a tailored quote.
X
We use cookies to offer you a better browsing experience, analyze site traffic and personalize content. By using this site, you agree to our use of cookies. Privacy Policy
RejectAccept